


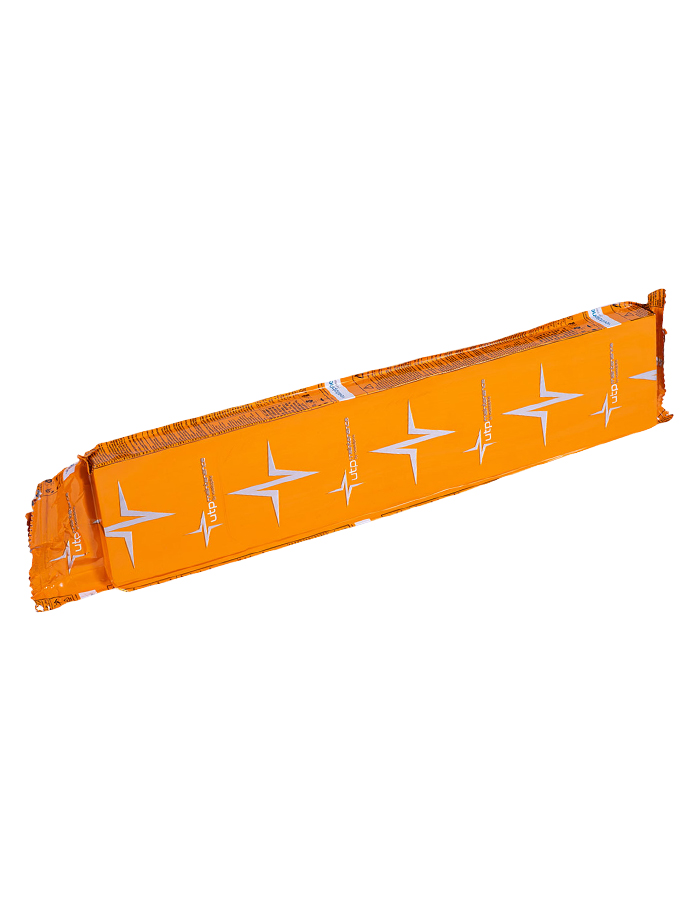
Electrodes BOHLER UTP 65 D 2.5x250mm/1.2kg (49362) (E312-17) Dry System 20

Do you need advice?
Electrodes BOHLER UTP 65 D 2.5x250mm/1.2kg (49362) (E312-17) Dry System 20
 Elektródy BOHLER UTP 65 D 1,6x250mm/2,9kg/267ks (45933) (E312-17)
61,50 € incl. tax
 Elektródy BOHLER UTP 65 D 2,0x250mm/3,1kg/302ks (15776) (E312-17)
58,43 € incl. tax
 Elektródy BOHLER UTP 65 D 3,2x350mm/4,7kg/140ks (16197) (E312-17)
41,29 € incl. tax
 Elektródy BOHLER UTP 65 D 2,5x250mm/3,4kg/246ks (15793) (E312-17)
47,79 € incl. tax
 Elektródy BOHLER UTP 65 D 2,5x250mm/1,2kg (49362) (E312-17) Dry System 20
70,73 € incl. tax
 Elektródy BOHLER UTP 65 D 3,2x350mm/1,3kg (49338) (E312-17) Dry System 15
66,05 € incl. tax
70,73 € incl. tax

BÖHLER UTP 65 D Electrodes - 2.5 × 250 mm / 1.2 kg / 49362 / E312-17 / Dry System 20
BÖHLER UTP 65 D are special rutile-coated austenitic-ferritic electrodes designed for repairs, surfacing and welding of difficult-to-weld steels. Thanks to their high resistance to cracking, they are suitable for demanding repair work where a strong, tough and reliable weld is required.
The electrodes are used primarily in the welding and repair of tool steels, spring steels, manganese steels, high-speed steels and for joining dissimilar materials, such as stainless steel to unalloyed or low-alloy steel. They are also used in the repair of shafts, gears, cams, moulds, cutting tools and machine parts.
The diameter of 2.5 mm is suitable for general repair use, medium-stress welds, surfacing and parts where good control over the weld pool is required. The Dry System 20 packaging helps protect the electrodes from moisture and keeps them ready for reliable use when stored correctly.
Main advantages:
- Special electrode for repairs and surfacing
- Suitable for difficult-to-weld steels
- Usable for tool, spring, manganese and high-speed steels
- Also suitable for joining dissimilar materials
- High resistance to cracking
- Good resistance to wear and corrosion
- Stable arc and good controllability
- Good slag removability
- Also suitable as an elastic intermediate layer under hardfacing
- Dry System 20 packaging for moisture protection
- Practical 1.2 kg pack
Mechanical properties of the weld metal
| Parameter | Typical value |
|---|---|
| Yield strength Rp0.2 | > 640 N/mm² |
| Tensile strength Rm | > 800 MPa |
| Elongation A5 | > 20 % |
| Hardness | approx. 260 HB |
Typical chemical composition of the weld metal
| Element | Value |
|---|---|
| C | 0,1 % |
| Si | 1,0 % |
| Mn | 1,0 % |
| Cr | 30,0 % |
| Ni | 9,5 % |
| Fe | balance |
Welding recommendation:
Before welding, it is necessary to thoroughly clean the welding area. For thicker parts, it is recommended to prepare a V or X weld groove and for high-carbon or massive parts, consider preheating to approximately 250 °C. The electrode should be guided with a short arc, either directly or with slight weaving, depending on the application.
In case of dampening, re-drying for 2 hours at a temperature of 120 – 200 °C is recommended.
BOHLER UTP 65 D Electrodes - 2.5x250mm / 1.2kg (49362) (E312-17) Dry System 20
Do you need advice?
Related products
Elektródy BOHLER UTP 65 D 2,0x250mm/3,1kg/302ks (15776) (E312-17)
58,43 € incl. tax
Elektródy BOHLER UTP 65 D 3,2x350mm/4,7kg/140ks (16197) (E312-17)
41,29 € incl. tax
Elektródy BOHLER UTP 65 D 2,5x250mm/3,4kg/246ks (15793) (E312-17)
47,79 € incl. tax
Elektródy BOHLER UTP 65 D 2,5x250mm/1,2kg (49362) (E312-17) Dry System 20
70,73 € incl. tax
Elektródy BOHLER UTP 65 D 3,2x350mm/1,3kg (49338) (E312-17) Dry System 15
66,05 € incl. tax
Electrodes BOHLER UTP 65 D 1.6x250mm/2.9kg/267pcs (45933) (E312-17)
61,50 € incl. tax
Elektródy BOHLER UTP 65 D 1,6x250mm/2,9kg/267ks (45933) (E312-17)
61,50 € incl. tax
Elektródy BOHLER UTP 65 D 3,2x350mm/4,7kg/140ks (16197) (E312-17)
41,29 € incl. tax
Elektródy BOHLER UTP 65 D 2,5x250mm/3,4kg/246ks (15793) (E312-17)
47,79 € incl. tax
Elektródy BOHLER UTP 65 D 2,5x250mm/1,2kg (49362) (E312-17) Dry System 20
70,73 € incl. tax
Elektródy BOHLER UTP 65 D 3,2x350mm/1,3kg (49338) (E312-17) Dry System 15
66,05 € incl. tax
Electrodes BOHLER UTP 65 D 2.0x250mm/3.1kg/302pcs (15776) (E312-17)
58,43 € incl. tax
Elektródy BOHLER UTP 65 D 1,6x250mm/2,9kg/267ks (45933) (E312-17)
61,50 € incl. tax
Elektródy BOHLER UTP 65 D 2,0x250mm/3,1kg/302ks (15776) (E312-17)
58,43 € incl. tax
Elektródy BOHLER UTP 65 D 2,5x250mm/3,4kg/246ks (15793) (E312-17)
47,79 € incl. tax
Elektródy BOHLER UTP 65 D 2,5x250mm/1,2kg (49362) (E312-17) Dry System 20
70,73 € incl. tax
Elektródy BOHLER UTP 65 D 3,2x350mm/1,3kg (49338) (E312-17) Dry System 15
66,05 € incl. tax
Electrodes BOHLER UTP 65 D 3.2x350mm/4.7kg/140pcs (16197) (E312-17)
41,29 € incl. tax
Alternative goods
Elektródy BOHLER UTP 65 D 1,6x250mm/2,9kg/267ks (45933) (E312-17)
61,50 € incl. tax
Elektródy BOHLER UTP 65 D 2,0x250mm/3,1kg/302ks (15776) (E312-17)
58,43 € incl. tax
Elektródy BOHLER UTP 65 D 2,5x250mm/3,4kg/246ks (15793) (E312-17)
47,79 € incl. tax
Elektródy BOHLER UTP 65 D 2,5x250mm/1,2kg (49362) (E312-17) Dry System 20
70,73 € incl. tax
Elektródy BOHLER UTP 65 D 3,2x350mm/1,3kg (49338) (E312-17) Dry System 15
66,05 € incl. tax
Electrodes BOHLER UTP 65 D 3.2x350mm/4.7kg/140pcs (16197) (E312-17)
41,29 € incl. tax
Elektródy BOHLER UTP 65 D 1,6x250mm/2,9kg/267ks (45933) (E312-17)
61,50 € incl. tax
Elektródy BOHLER UTP 65 D 3,2x350mm/4,7kg/140ks (16197) (E312-17)
41,29 € incl. tax
Elektródy BOHLER UTP 65 D 2,5x250mm/3,4kg/246ks (15793) (E312-17)
47,79 € incl. tax
Elektródy BOHLER UTP 65 D 2,5x250mm/1,2kg (49362) (E312-17) Dry System 20
70,73 € incl. tax
Elektródy BOHLER UTP 65 D 3,2x350mm/1,3kg (49338) (E312-17) Dry System 15
66,05 € incl. tax
Electrodes BOHLER UTP 65 D 2.0x250mm/3.1kg/302pcs (15776) (E312-17)
58,43 € incl. tax
Elektródy BOHLER UTP 65 D 1,6x250mm/2,9kg/267ks (45933) (E312-17)
61,50 € incl. tax
Elektródy BOHLER UTP 65 D 2,0x250mm/3,1kg/302ks (15776) (E312-17)
58,43 € incl. tax
Elektródy BOHLER UTP 65 D 3,2x350mm/4,7kg/140ks (16197) (E312-17)
41,29 € incl. tax
Elektródy BOHLER UTP 65 D 2,5x250mm/1,2kg (49362) (E312-17) Dry System 20
70,73 € incl. tax
Elektródy BOHLER UTP 65 D 3,2x350mm/1,3kg (49338) (E312-17) Dry System 15
66,05 € incl. tax
Electrodes BOHLER UTP 65 D 2.5x250mm/3.4kg/246pcs (15793) (E312-17)
47,79 € incl. tax
Elektródy BOHLER UTP 65 D 2,0x250mm/3,1kg/302ks (15776) (E312-17)
58,43 € incl. tax
Elektródy BOHLER UTP 65 D 3,2x350mm/4,7kg/140ks (16197) (E312-17)
41,29 € incl. tax
Elektródy BOHLER UTP 65 D 2,5x250mm/3,4kg/246ks (15793) (E312-17)
47,79 € incl. tax
Elektródy BOHLER UTP 65 D 2,5x250mm/1,2kg (49362) (E312-17) Dry System 20
70,73 € incl. tax
Elektródy BOHLER UTP 65 D 3,2x350mm/1,3kg (49338) (E312-17) Dry System 15
66,05 € incl. tax
Electrodes BOHLER UTP 65 D 1.6x250mm/2.9kg/267pcs (45933) (E312-17)
61,50 € incl. tax
Elektródy BOHLER UTP 65 D 1,6x250mm/2,9kg/267ks (45933) (E312-17)
61,50 € incl. tax
Elektródy BOHLER UTP 65 D 2,0x250mm/3,1kg/302ks (15776) (E312-17)
58,43 € incl. tax
Elektródy BOHLER UTP 65 D 3,2x350mm/4,7kg/140ks (16197) (E312-17)
41,29 € incl. tax
Elektródy BOHLER UTP 65 D 2,5x250mm/3,4kg/246ks (15793) (E312-17)
47,79 € incl. tax
Elektródy BOHLER UTP 65 D 3,2x350mm/1,3kg (49338) (E312-17) Dry System 15
66,05 € incl. tax
Electrodes BOHLER UTP 65 D 2.5x250mm/1.2kg (49362) (E312-17) Dry System 20
70,73 € incl. tax
Elektródy BOHLER UTP 65 D 1,6x250mm/2,9kg/267ks (45933) (E312-17)
61,50 € incl. tax
Elektródy BOHLER UTP 65 D 2,0x250mm/3,1kg/302ks (15776) (E312-17)
58,43 € incl. tax
Elektródy BOHLER UTP 65 D 3,2x350mm/4,7kg/140ks (16197) (E312-17)
41,29 € incl. tax
Elektródy BOHLER UTP 65 D 2,5x250mm/3,4kg/246ks (15793) (E312-17)
47,79 € incl. tax
Elektródy BOHLER UTP 65 D 2,5x250mm/1,2kg (49362) (E312-17) Dry System 20
70,73 € incl. tax
Electrodes BOHLER UTP 65 D 3.2x350mm/1.3kg (49338) (E312-17) Dry System 15
66,05 € incl. tax
Do you need advice?


Lieskovská cesta 13
962 21 Lieskovec





