


Pipe wire. MIG BOHLER Q Zn GS 1.2mm /250kg (61981)

Do you need advice?
Pipe wire. MIG BOHLER Q Zn GS 1.2mm /250kg (61981)
7,31 € incl. tax

BÖHLER Q Zn GS MIG tubular wire 1.2 mm / 250 kg (61981)
BÖHLER Q Zn GS is a special metal-cored welding wire designed for MAG welding of galvanised and hot-dip galvanised steel sheets. It is primarily developed for single-pass welding of galvanised sheets with a thickness of up to 4 mm. Its composition and arc characteristics help reduce porosity, spatter, and the need for subsequent cleaning of the weld joints.
The wire complies with the EN ISO 17632-A: T 3 T Z M M21 1 and AWS A5.18: E70C-GS classifications. Thanks to the special metal-cored filling, it provides good welding properties even at lower welding parameters, stable electric arc combustion and good wetting of the weld edges.
When welding galvanised sheets, zinc evaporation can cause porosity and instability in the welding process. BÖHLER Q Zn GS is designed to help limit these issues and enable the creation of high-quality welds while maintaining good productivity. It features low spatter formation, a good weld bead appearance, and easy removal of slag residue during single-pass welding.
A wider electric arc and good wetting of the weld edges help compensate for minor inaccuracies when assembling sheet metal parts. The wire is suitable for fillet and lap weld joints, where a uniform weld, good repeatability and a reduction in subsequent finishing operations are required.
Main areas of application include the automotive industry, bodywork manufacturing, galvanised sheet metal structures, HVAC systems, sheet metal covers, thin-walled profiles and light steel assemblies. The wire is particularly suitable for workshops that regularly weld parts with a zinc surface finish.
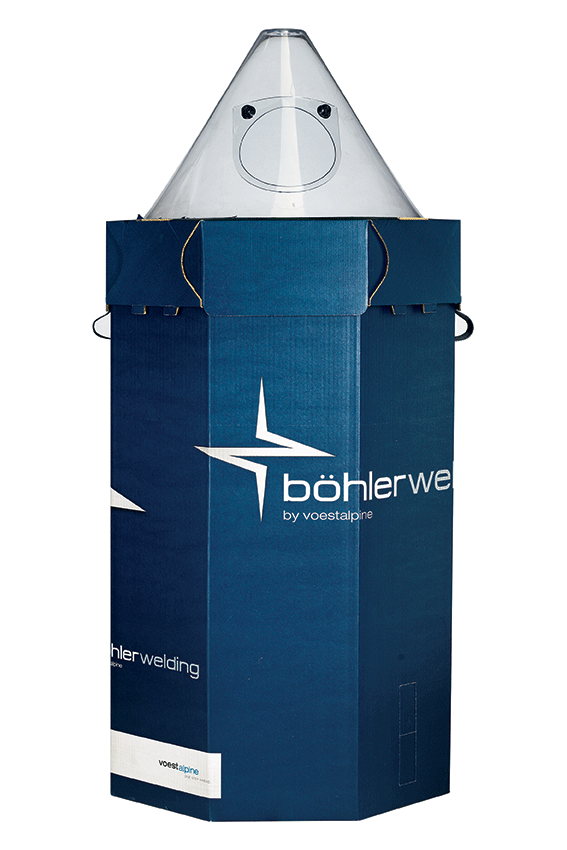
A significant advantage of the 61981 variant is the high-capacity BASEdrum packaging containing 250 kg of welding wire. The packaging is primarily intended for series, mechanised, automated, and robotic production. Compared to standard 16 kg spools, it significantly reduces the number of packaging changes and welding station downtime.
A compatible welding wire unwinding and guiding system is required to use the drum packaging. The wire is not fed from a classic BS300 spool, but from a high-capacity drum through suitable accessories into the feeding mechanism of the welding equipment. The specific accessories must be selected according to the type of drum and the welding workstation.
Welding is performed using the MAG process with metal-cored wire (138). The manufacturer prescribes shielding gas Ar + 5–25 % CO2 according to EN ISO 14175, group M20 or M21. The wire requires negative polarity DC−, meaning the welding wire is connected to the negative pole of the power source. This is not a self-shielding flux-cored wire and a prescribed shielding gas must be used during welding.
For a diameter of 1.2 mm, the manufacturer recommends a welding current of 160–220 A, a voltage of 17–21 V, and a wire feed speed of 3.5–5.5 m/min. The parameters are primarily intended for galvanised sheets with a thickness of 2–4 mm. The recommended wire stick-out is 15–20 mm, and the manufacturer recommends push torch guidance.
When welding galvanised materials, it is essential to ensure effective extraction of welding fumes, as the process generates vapours containing zinc compounds. After welding, it is advisable to restore the anti-corrosion protection in areas where the zinc layer has been damaged by heat.
BÖHLER Q Zn GS 1.2 mm / 250 kg represents a productive solution for industrial sites focused on welding galvanised steel parts requiring a stable process, low spatter, and minimal downtime during welding material replacement.
Main advantages:
- Professional welding wire BÖHLER Q Zn GS
- Special tubular wire with metal fill – metal-cored
- Designed for welding galvanised and hot-dip galvanised steel sheets
- Optimised for single-pass welding of sheets up to 4 mm
- Reduced risk of porosity in the weld metal
- Stable electric arc even at lower welding parameters
- Low spatter formation
- Easier removal of spatter from galvanised surfaces
- Good wetting of weld edges
- Uniform and aesthetic appearance of the weld bead
- Easy removal of slag residues after single-pass welding
- Good bridging of minor assembly inaccuracies
- Suitable for fillet and lap joints
- Capable of achieving high welding speeds
- Reduced need for post-weld cleaning
- Application in the manufacture of automotive bodies
- Suitable for HVAC and air conditioning systems
- High-capacity BASEdrum 250 kg packaging
- Reduced downtime during welding material replacement
- Suitable for automated and robotic welding workstations
- Shielding gas M20/M21 – Ar + 5–25 % CO2
- Welding with negative polarity DC−
- Recommended welding current 160–220 A
- Recommended voltage 17–21 V
- Wire diameter 1.2 mm
Classification:
| Standard / Designation | Classification |
|---|---|
| EN ISO 17632-A | T 3 T Z M M21 1 |
| AWS A5.18 / SFA-5.18 | E70C-GS |
| Trade name | BÖHLER Q Zn GS |
| Welding wire type | Metal-cored |
| Welding process | MAG 138 |
| Shielding gas | M20 / M21 |
| Polarity | DC− |
| Manufacturer code | 61981 |
| Packaging | BASEdrum 250 kg |
Chemical composition of weld metal:
| Chemical element | Typical content (%) |
|---|---|
| Carbon (C) | 0,30 |
| Silicon (Si) | 0,30 |
| Manganese (Mn) | 1,10 |
| Aluminium (Al) | 1,80 |
| Iron (Fe) | Remainder and other accompanying elements |
Typical chemical composition of the pure weld metal using M20/M21 shielding gas according to BÖHLER Q Zn GS. Values do not represent an analysis of a specific production batch.
Mechanical properties:
| Mechanical property | Value according to manufacturer |
|---|---|
| Yield strength Rp0.2 | > 355 MPa |
| Tensile strength Rm | > 490 MPa |
| Elongation A5 | Not specified |
| Impact energy KV | Not specified |
| Weld metal condition | As-welded, without heat treatment |
| Shielding gas during test | M20 / M21 |
Reference mechanical properties of the pure weld metal according to the BÖHLER Q Zn GS manufacturer's technical data sheet (2021).
Do you need advice?
Do you need advice?


Lieskovská cesta 13
962 21 Lieskovec





