


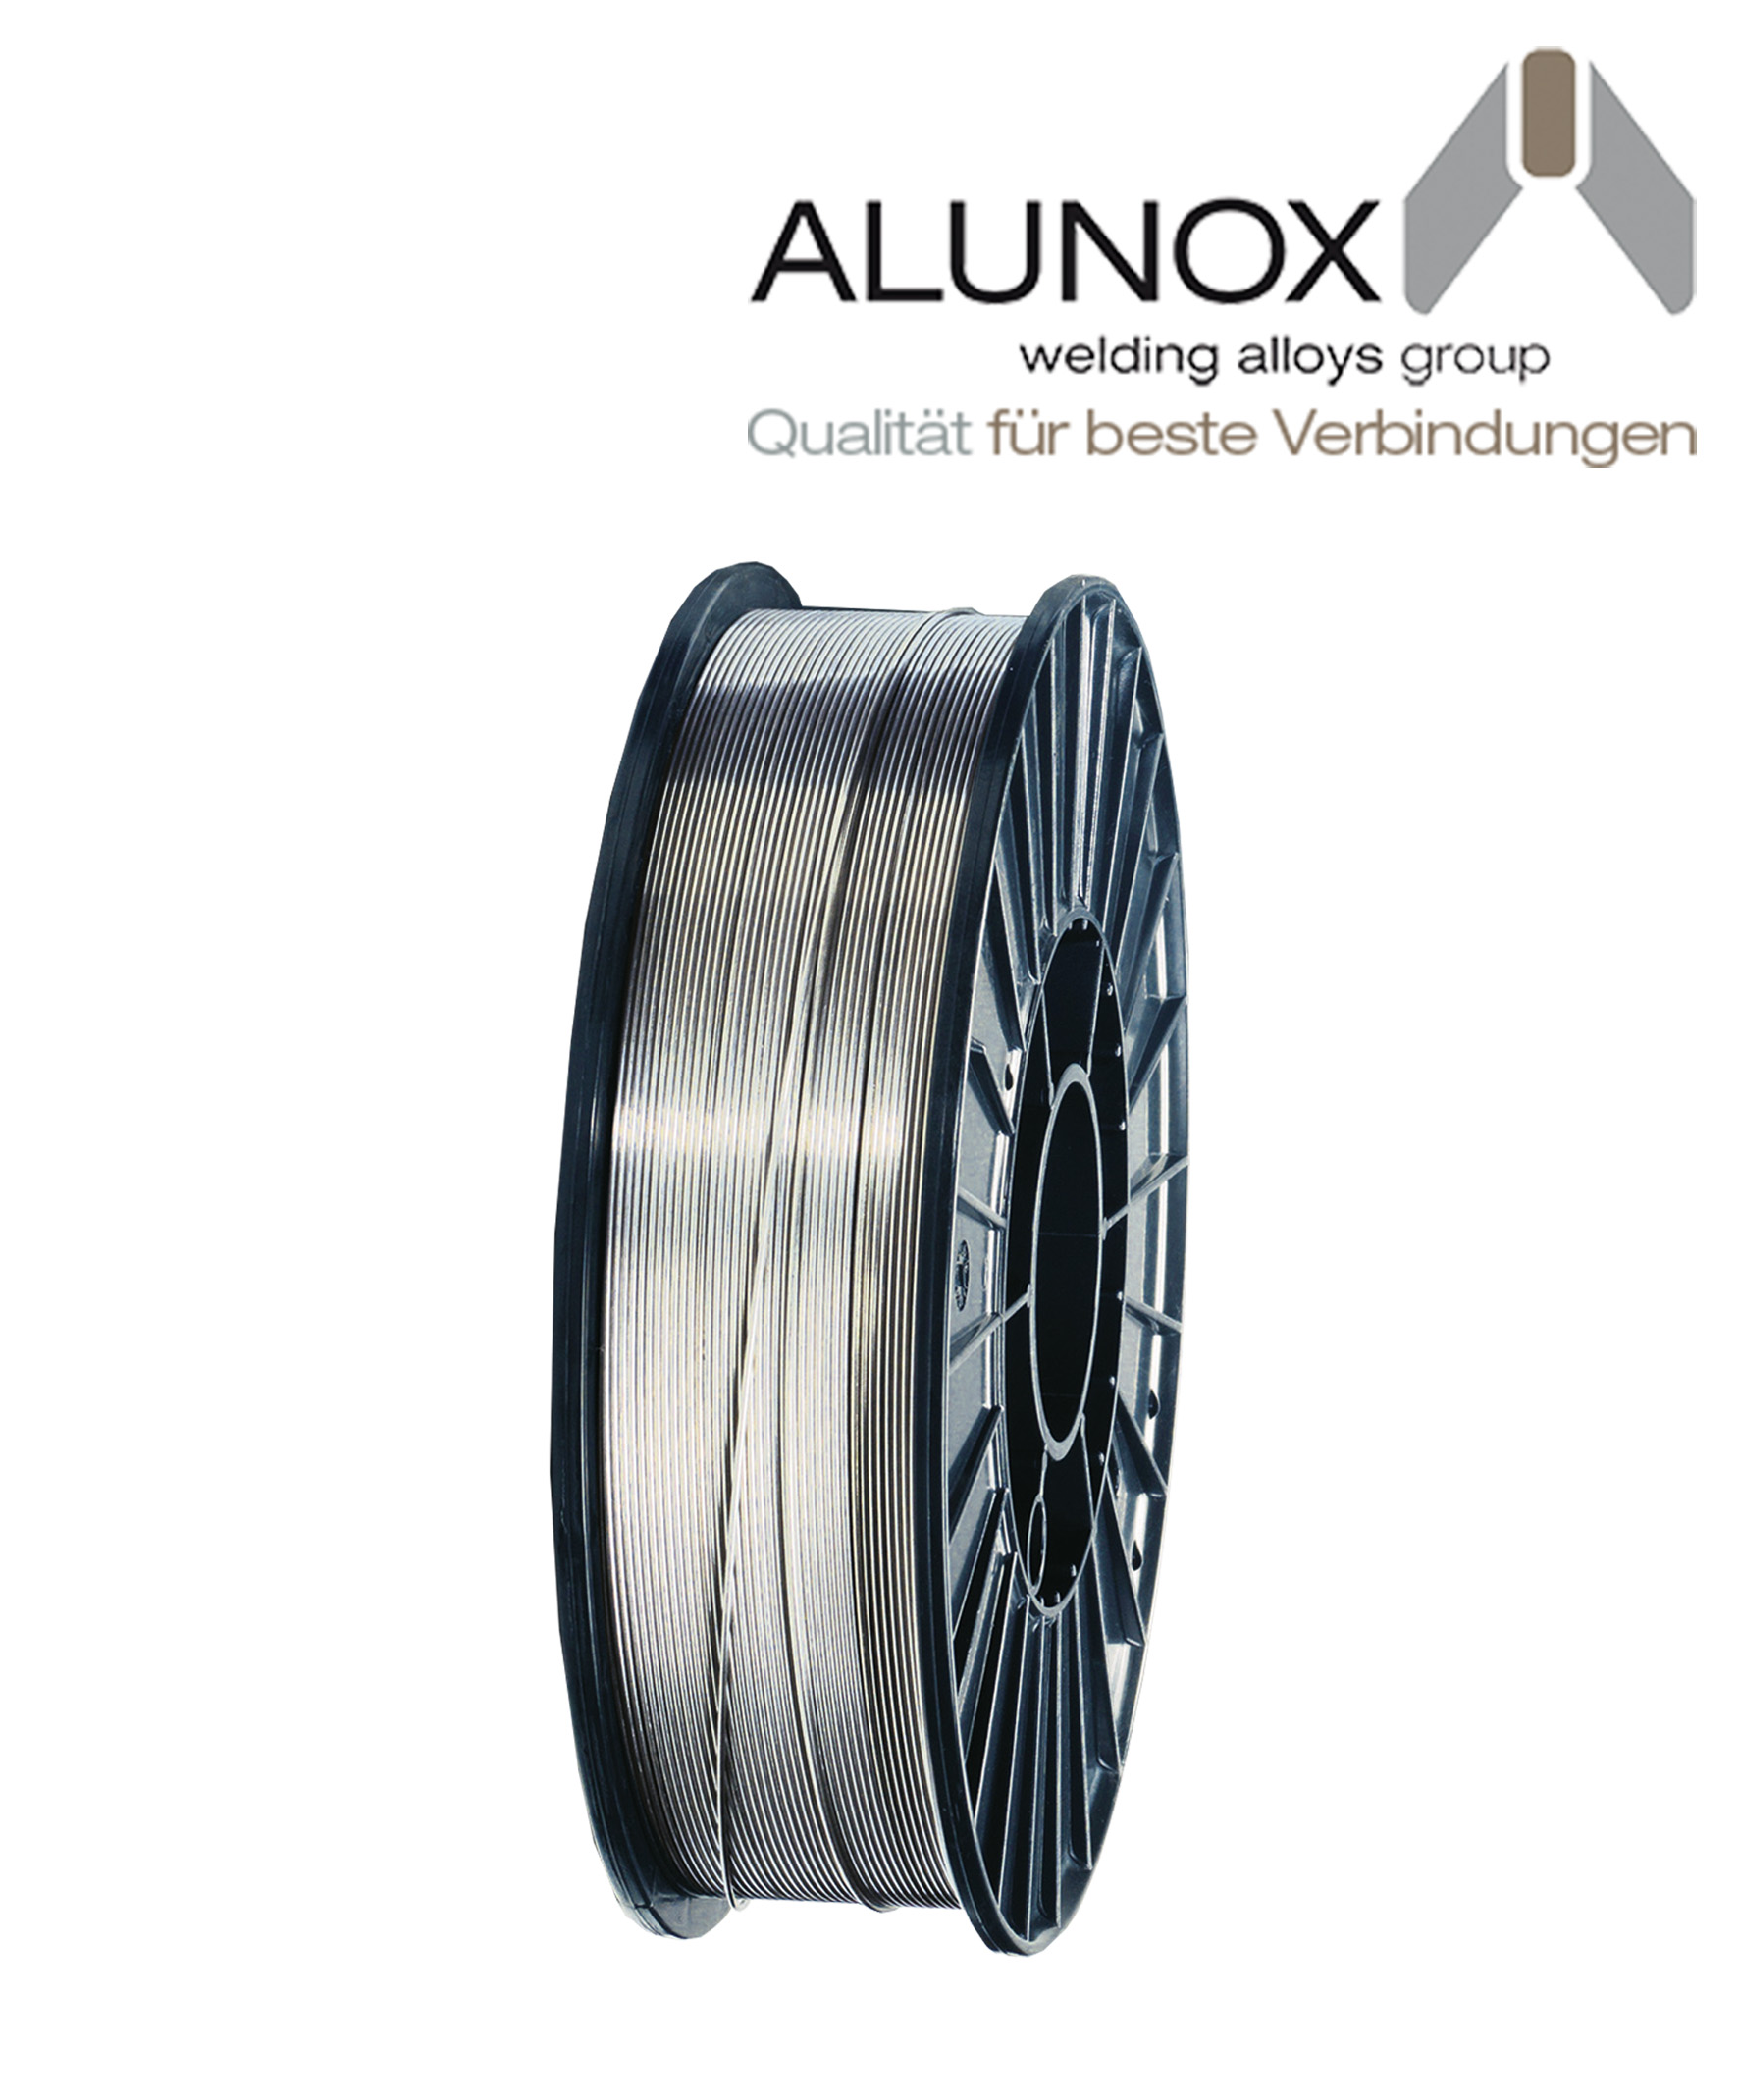
MIG wire ALUNOX 308LSi 1.0mm /5kg (1.4316)

Do you need advice?
MIG wire ALUNOX 308LSi 1.0mm /5kg (1.4316)
 Drôt MIG ALUNOX 308LSi 0,8mm/5kg (1.4316)
24,26 € incl. tax
 Drôt MIG ALUNOX 308LSi 1,0mm /5kg (1.4316)
22,44 € incl. tax
22,44 € incl. tax

ALUNOX 308LSi MIG Wire 1.0 mm / 5 kg / 1.4316
ALUNOX 308LSi MIG wire is a high-alloy austenitic stainless steel welding wire intended for MIG/MAG welding of chromium-nickel steels, primarily types AISI 304 and 304L. It corresponds to classification ER308LSi / G 19 9 L Si / 1.4316. Thanks to its low carbon content, it provides good resistance to intergranular corrosion, while the increased silicon content ensures excellent weld metal flow, a stable welding arc, and a smooth weld bead appearance.
The wire produces an austenitic weld metal with a delta ferrite content and, according to the manufacturer, is resistant to intergranular corrosion at operating temperatures up to 350 °C. It is also suitable for selected cryogenic applications at temperatures down to –196 °C, provided the requirements of the specific weld joint are met. It features good feedability and a stable welding process.
It is used in the production and repair of stainless steel pipes, tanks, reservoirs, process equipment and structures in the chemical, food, textile and engineering industries. It is suitable for welding steels EN 1.4301, 1.4306, 1.4311, 1.4541 and 1.4550 and other compatible austenitic stainless materials. The 1.0 mm diameter provides a good compromise between welding precision and deposition rate for thin to medium-thickness materials. The 5 kg pack is practical for use in workshops, service centres, metal fabrication, and for lower welding material consumption.
Main advantages:
- Stainless steel welding wire ALUNOX 308LSi for MIG/MAG welding
- Classification ER308LSi / G 19 9 L Si / 1.4316
- Suitable for welding austenitic steels AISI 304 and 304L
- Low carbon content for good resistance to intercrystalline corrosion
- Increased silicon content for very good weld metal flow
- Stable welding arc and smooth weld seam appearance
- Good feeding properties during mechanised welding
- Resistance to intergranular corrosion at operating temperatures up to 350 °C
- Suitable for selected cryogenic applications down to –196 °C
- Suitable for the production of pipes, tanks, and process equipment
- Diameter 1.0 mm for thin and medium-thickness materials
- Practical 5 kg pack
Classification:
| Standard / Designation | Classification |
|---|---|
| AWS A5.9 | ER308LSi |
| EN ISO 14343-A | G 19 9 L Si |
| EN ISO 14343-B | SS308LSi |
| W.Nr. / material number | 1.4316 |
| Filler material type | Solid high-alloy austenitic stainless steel welding wire |
| Welding process | MIG/MAG (135 with active shielding gas) |
Chemical composition:
| Chemical element | Content (%) |
|---|---|
| Carbon (C) | 0,02 |
| Silicon (Si) | 0,90 |
| Manganese (Mn) | 1,80 |
| Chromium (Cr) | 19,70 |
| Nickel (Ni) | 9,20 |
Typical chemical composition of the wire according to the ALUNOX technical data sheet. This is not a chemical analysis of a specific production batch.
Mechanical properties:
| Mechanical property | Typical value |
|---|---|
| Yield strength Rp0.2 | 420 MPa |
| Tensile strength Rm | 620 MPa |
| Elongation A (L0 = 5d0) | 35 % |
| Impact energy KV (+20 °C) | 100 J |
Typical mechanical properties of the pure weld metal according to ALUNOX. The manufacturer states these values with 100% argon shielding gas, without subsequent heat treatment. Actual properties when MAG welding with mixed gases may vary.
Do you need advice?
Do you need advice?


Lieskovská cesta 13
962 21 Lieskovec





