


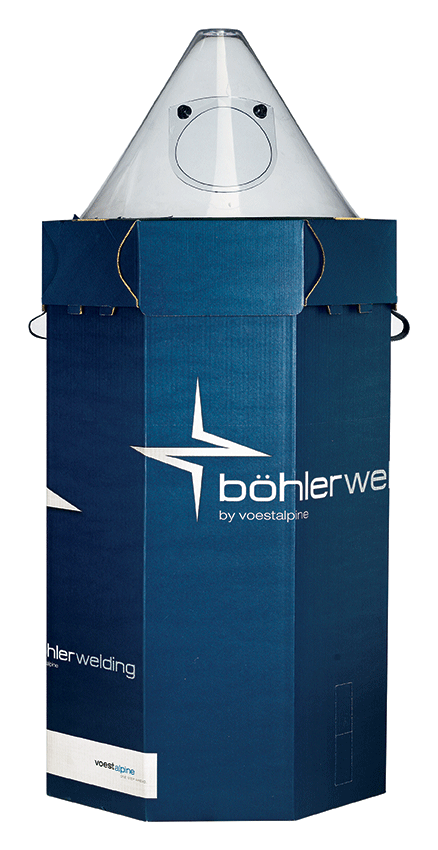
MIG wire BOHLER DMV 83-IG 1.2mm /18kg (27695)

Do you need advice?
MIG wire BOHLER DMV 83-IG 1.2mm /18kg (27695)
26,85 € incl. tax

MIG Wire BÖHLER DMV 83-IG 1.2 mm / 18 kg (27695)
BÖHLER DMV 83-IG is a professional low-alloy solid welding wire alloyed with chromium, molybdenum, and vanadium (Cr-Mo-V), designed for MAG welding of heat-resistant steels resistant to creep at elevated temperatures. It corresponds to classification EN ISO 21952-A: G MoVSi and is listed in the manufacturer's current catalogue according to AWS A5.28: ER80S-G. The material number of the filler material is 1.5407.
The welding wire is specifically developed for welding 14MoV6-3 (1.7715) steel and similar heat-resistant alloy steels used in the production of boilers, pressure vessels, and piping systems. The alloying elements chromium (Cr), molybdenum (Mo), and vanadium (V) ensure the required weld metal properties under long-term thermal and mechanical stress. The weld metal is characterised by good toughness, resistance to cracking, and high creep strength.
BÖHLER DMV 83-IG is intended for use in the energy sector, heating engineering, and the production of steam boilers, pressure equipment, and high-temperature piping. According to the manufacturer's technical data, it is suitable for applications with a long-term operating temperature of up to +560 °C, provided that the relevant design, material, and technological requirements are met.
The wire provides very good feeding properties, smooth welding, and good wetting of the weld seams. It is used for solid wire welding using the MAG (135) process with a shielding mixture of argon and carbon dioxide, specifically Ar + 15–25 % CO2, or pure CO2 according to the approved technological procedure. Welding is carried out using direct current with positive wire polarity DC+.
When welding heat-resistant steels, it is important to adhere to the recommended preheating temperature and interpass temperature of 200–300 °C. The manufacturer recommends subsequent heat treatment of the weld joint at 700–720 °C for at least 2 hours, followed by furnace cooling to approximately 300 °C and then air cooling. The specific procedure must correspond to the base material, wall thickness, and approved welding procedure.
The 1.2 mm diameter is suitable for the professional welding of pipes, boiler parts, pressure equipment, and other components made of heat-resistant steels. The wire is supplied on an 18 kg spool for industrial MIG/MAG welding equipment.
Main advantages:
- Professional heat-resistant welding wire BÖHLER DMV 83-IG
- Low-alloy solid wire with Cr-Mo-V alloying
- Classification EN ISO 21952-A: G MoVSi
- Current catalogue designation AWS ER80S-G
- Specifically designed for welding heat-resistant steel 14MoV6-3 (1.7715)
- High creep resistance of the weld metal at elevated temperatures
- Good toughness and resistance to cracking
- Suitable for long-term operating temperatures up to 560 °C according to the technical data sheet
- Very good wire feeding properties
- Smooth welding and good wetting of the weld edges
- Suitable for the manufacture and repair of steam boilers
- Used for welding pressure vessels and high-temperature piping
- Applications in power engineering and district heating
- Option to use Ar/CO2 or CO2 shielding gas according to the procedure
- Direct current welding DC+
- Recommended preheating and interpass temperature 200–300 °C
- Diameter 1.2 mm for professional MAG welding
- Industrial packaging 18 kg on spool
Classification:
| Standard / Designation | Classification |
|---|---|
| EN ISO 21952-A | G MoVSi |
| AWS A5.28 / SFA-5.28 | ER80S-G – current online catalogue |
| Material number | 1.5407 |
| Trade name | BÖHLER DMV 83-IG |
| Material group | Low-alloy heat-resistant Cr-Mo-V steel |
| Filler material type | Solid steel welding wire |
| Welding process | MAG (135) |
| Polarity | DC+ |
Chemical composition:
| Chemical element | Typical content (%) |
|---|---|
| Carbon (C) | 0,08 |
| Silicon (Si) | 0,60 |
| Manganese (Mn) | 0,90 |
| Chromium (Cr) | 0,45 |
| Molybdenum (Mo) | 0,82 |
| Vanadium (V) | 0,35 |
| Iron (Fe) | Balance |
Typical chemical composition of the solid wire according to the BÖHLER DMV 83-IG technical data sheet. Values do not represent a chemical analysis of a specific production batch.
Mechanical properties:
| Mechanical property | Typical value | Minimum value |
|---|---|---|
| Yield strength Rp0.2 | 610 MPa | 355 MPa |
| Tensile strength Rm | 710 MPa | 620 MPa |
| Elongation A5 | 20 % | 18 % |
| Impact energy KV (+20 °C) | 70 J | 47 J |
| Weld metal condition | After heat treatment at 700 °C for 2 hours | |
| Shielding gas during test | Ar + 18 % CO2 | |
Mechanical properties of the pure weld metal according to the BÖHLER DMV 83-IG technical data sheet, after annealing at 700 °C for 2 hours with furnace cooling to 300 °C followed by air cooling. The stated minimum values are reference values in the documentation, not a test certificate of the delivered batch.
Do you need advice?
Alternative goods


MIG wire ER80S-G 1.2mm/16kg CORTEN
5,61 € incl. tax
Do you need advice?


Lieskovská cesta 13
962 21 Lieskovec





