


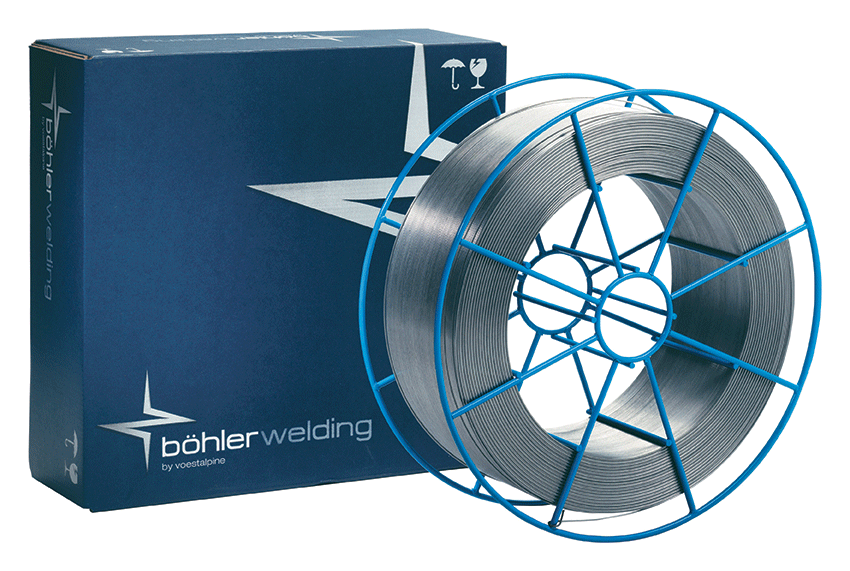
MIG wire BOHLER QG 307 1.2mm /15kg (72102) ER307 18 8 Mn

Do you need advice?
MIG wire BOHLER QG 307 1.2mm /15kg (72102) ER307 18 8 Mn
 Drôt MIG BOHLER Q G 307 1,0mm /15kg (72086) ER307 18 8 Mn
19,09 € incl. tax
 Drôt MIG BOHLER Q G 307 1,2mm /15kg (72102) ER307 18 8 Mn
18,57 € incl. tax
 Drôt MIG BOHLER Q G 307 1,6mm /15kg (72088) ER307 18 8 Mn
19,85 € incl. tax
18,57 € incl. tax

BÖHLER Q G 307 MIG Wire 1.2 mm / 15 kg / 1.4370 / BS300 (72102)
BÖHLER Q G 307 MIG wire is a high-alloy austenitic welding wire designed for MIG/MAG welding of dissimilar and difficult-to-weld steels, heat-resistant chromium and chromium-nickel steels, and castings. Thanks to its Cr-Ni-Mn chemical composition with approximately 19% chromium, 9% nickel, and 7% manganese, it provides a tough weld metal with good ductility and resistance to cracking under mechanical stress.
It is used for welding combinations of structural, fine-grained, refined, and high-alloy steels. It is particularly suitable for joining austenitic and ferritic materials, repair welding, and creating tough buffer layers prior to hardfacing. It is applied in the repair of machine parts, steel structures, and industrial equipment. The 1.2 mm diameter is suitable for welding medium-to-thick materials and allows for a higher deposition rate. The 15 kg BS300-BLUE spool is designed for professional use in metal fabrication, maintenance, and industrial operations.
Main advantages:
- High-alloy austenitic MIG/MAG wire BÖHLER Q G 307
- Suitable for welding dissimilar and difficult-to-weld steels
- Suitable for joints between austenitic and ferritic steels
- Suitable for welding and surfacing of heat-resistant steels and castings
- Higher manganese content for good toughness and ductility of the weld metal
- Suitable for repair welding and tough buttering layers before hardfacing
- Applicable to selected heat-resistant steels up to 850 °C according to the manufacturer
- Diameter 1.2 mm for higher welding performance and welding of thicker materials
- Compatible with shielding gases M12, M13 and M21
- Approvals TÜV, DB and CE
Classification:
| Standard / Designation | Classification |
|---|---|
| AWS A5.9 / SFA-5.9 | ER307 (mod.) |
| EN ISO 14343-A | G 18 8 Mn |
| W.Nr. / material number | 1.4370 |
| Filler material type | Solid high-alloy austenitic welding wire |
| Welding process | MIG/MAG |
Chemical composition:
| Chemical element | Content (%) |
|---|---|
| Carbon (C) | 0,08 |
| Silicon (Si) | 0,8 |
| Manganese (Mn) | 7,0 |
| Chromium (Cr) | 19,0 |
| Nickel (Ni) | 9,0 |
Typical chemical composition according to the BÖHLER Welding technical data sheet.
Mechanical properties:
| Mechanical property | Typical value |
|---|---|
| Yield strength Rp0.2 | 430 MPa |
| Tensile strength Rm | 640 MPa |
| Elongation A (L0 = 5d0) | 36 % |
| Impact energy KV (+20 °C) | 100 J |
| Impact energy KV (-110 °C) | min. 32 J |
Typical mechanical properties of the pure weld metal in the as-welded condition using Ar + 2.5% CO2 shielding gas. Values according to the BÖHLER Welding technical data sheet.
Do you need advice?
Do you need advice?


Lieskovská cesta 13
962 21 Lieskovec





