


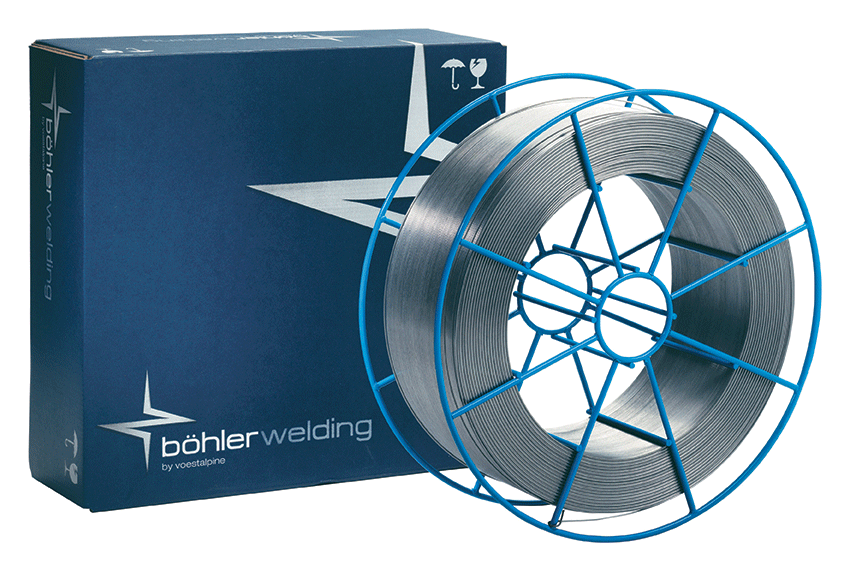
MIG wire BOHLER Thermanit H-347Si 1.0mm /15kg (ER347Si) (17864)

Do you need advice?
MIG wire BOHLER Thermanit H-347Si 1.0mm /15kg (ER347Si) (17864)
 Drôt MIG BOHLER Thermanit H-347Si 0,8mm /15kg (ER347Si) (53184)
29,95 € incl. tax
 Drôt MIG BOHLER Thermanit H-347Si 1,0mm /15kg (ER347Si) (17864)
28,78 € incl. tax
 Drôt MIG BOHLER Thermanit H-347Si 1,2mm /15kg (ER347Si) (13404)
28,41 € incl. tax
28,78 € incl. tax

BÖHLER Thermanit H-347Si MIG Wire 1.0 mm / 15 kg (ER347Si) – 17864
BÖHLER Thermanit H-347Si is a high-alloy solid stainless steel welding wire designed for MAG welding of stabilised and non-stabilised austenitic stainless steels. It corresponds to classification AWS A5.9: ER347Si and EN ISO 14343-A: G 19 9 Nb Si. The material number of the filler metal is 1.4551.
The wire is alloyed with chromium, nickel, and niobium, with a chemical composition containing approximately 19.5% chromium and 9.5% nickel. Niobium stabilises the weld metal and restricts the formation of chromium carbides, contributing to resistance against intergranular corrosion. The increased silicon content improves the flowability of the molten metal, the wetting of the weld joints, and the uniform appearance of the weld bead.
Thermanit H-347Si is primarily intended for welding titanium- and niobium-stabilised austenitic steels 1.4541 (AISI 321), 1.4546, and 1.4550 (AISI 347). It can also be used for compatible steels 1.4301 (AISI 304), 1.4306 (AISI 304L), 1.4311 (AISI 304LN) and selected stainless steel castings.
The weld metal is characterised by good strength, ductility, and toughness. The manufacturer states a possibility of use at low temperatures down to -196 °C and a maximum operating temperature of 400 °C. Application at these temperatures must correspond to the required mechanical properties, the base material, and a qualified welding procedure specification.
The welding wire is used in the production and repair of stainless steel pipes, tanks, reservoirs, pressure vessels, process piping, heat exchangers, valves, and industrial equipment. It is suitable for applications in the chemical, petrochemical, food, energy, and mechanical engineering industries.
Welding is performed using the MAG (135) process with shielding gases from groups M12 or M13 according to EN ISO 14175. The manufacturer specifies reference mechanical properties using the shielding gas mixture Ar + 2.5% CO2. Direct current with positive wire polarity DC+ is used.
When welding common austenitic stainless steels, preheating is generally not required. Subsequent heat treatment is mostly unnecessary. Welded surfaces must be free from grease, impurities, and foreign metal particles. For pipe joints, appropriate root protection of the weld must be ensured depending on the required quality.
A diameter of 1.0 mm provides good control of the weld pool and is suitable for welding thinner and medium-thickness stainless steel parts. The wire is supplied in 15 kg spools for professional and industrial MIG/MAG welding equipment.
Main advantages:
- Professional welding wire BÖHLER Thermanit H-347Si
- Classification AWS ER347Si / EN ISO G 19 9 Nb Si
- Material number 1.4551
- Designed for MAG welding of austenitic stainless steels
- Particularly suitable for stabilised steels AISI 321 and 347
- Option to weld compatible steels 304, 304L and 304LN
- Alloying of approximately 19.5% Cr and 9.5% Ni
- Niobium stabilisation limiting intergranular corrosion
- Increased silicon content improving the flowability of the weld metal
- Good wetting of weld edges
- Uniform and high-quality appearance of the weld bead
- Good feeding properties and stable welding process
- Good strength and ductility of the weld metal
- High toughness even at low temperatures
- Suitable for use at temperatures down to -196 °C
- Maximum operating temperature according to the manufacturer 400 °C
- Suitable for stainless steel pipes, tanks and pressure equipment
- Application in the chemical and petrochemical industries
- Shielding gases of groups M12 and M13
- Direct current welding DC+
- Diameter 1.0 mm for professional MAG welding
- Industrial packaging 15 kg on a spool
Classification:
| Standard / Designation | Classification |
|---|---|
| EN ISO 14343-A | G 19 9 Nb Si |
| EN ISO 14343-B | SS347Si |
| AWS A5.9 / SFA-5.9 | ER347Si |
| Material number | 1.4551 |
| Trade name | BÖHLER Thermanit H-347Si |
| Weld metal type | Niobium stabilised austenitic Cr-Ni |
| Welding process | MAG (135) |
| Shielding gas | M12 / M13 |
| Polarity | DC+ |
Chemical composition:
| Chemical element | Typical content (%) |
|---|---|
| Carbon (C) | 0,05 |
| Silicon (Si) | 0,80 |
| Manganese (Mn) | 1,50 |
| Chromium (Cr) | 19,50 |
| Nickel (Ni) | 9,50 |
| Niobium (Nb) | Min. 12 times the carbon content |
| Iron (Fe) | Balance |
Typical chemical composition according to the BÖHLER Thermanit H-347Si technical data sheet (07/2019). The values given do not represent an analysis of a specific production batch.
Mechanical properties:
| Mechanical property | Typical value | Minimum value |
|---|---|---|
| Yield strength Rp0.2 | 400 MPa | 350 MPa |
| Tensile strength Rm | 570 MPa | 550 MPa |
| Elongation A5 | 30 % | 25 % |
| Impact energy KV (+20 °C) | 100 J | Not specified |
| Impact energy KV (-196 °C) | 45 J | 32 J |
| Weld metal condition | As-welded, without additional heat treatment | |
| Shielding gas during test | Ar + 2.5 % CO2 | |
Mechanical properties of the pure weld metal according to the manufacturer's technical data sheet from July 2019. These are reference values under the specified conditions, not a test certificate for a specific batch.
Do you need advice?
Alternative goods
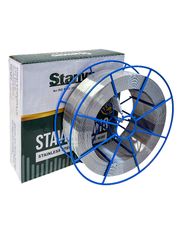
MIG wire STAVINOX ER 347Si 1.0mm/15kg (1.4551) BS300
8,98 € incl. tax
Do you need advice?


Lieskovská cesta 13
962 21 Lieskovec





