


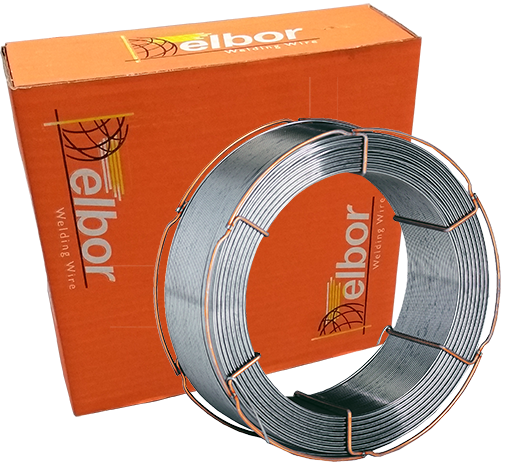
MIG wire ELBOR NiMoCr 1.0mm /16kg (ER110 SG)

Do you need advice?
MIG wire ELBOR NiMoCr 1.0mm /16kg (ER110 SG)
| Quantity | PriceUnit price | Discount % |
|---|---|---|
| 80544kg | 430,14 €5,38 € | 6% |
| 5451152kg | 2 680,96 €4,92 € | 14% |
| 11533456kg | 5 473,98 €4,75 € | 17% |
| 3457∞kg | 15 819,23 €4,58 € | 20% |
5,72 € incl. tax

MIG wire ELBOR NiMoCr 1.0 mm / 16 kg (ER110S-G) D300
ELBOR NiMoCr MIG wire is a low-alloy solid welding wire alloyed with nickel, molybdenum, and chromium, designed for MAG welding of high-strength, fine-grained, and refined structural steels. It complies with the AWS A5.28: ER110S-G designation and is intended for creating high-strength welded joints with good toughness even at low temperatures.
Alloying elements nickel (Ni), molybdenum (Mo), and chromium (Cr) help achieve the required strength, toughness, and mechanical properties of the weld metal. The wire is suitable for welding steel parts exposed to high mechanical stress, where maintaining the strength and reliability of the welded joint is essential. The weld metal is also intended for applications requiring impact toughness at temperatures down to approximately -40 °C.
ELBOR NiMoCr is used for welding high-strength steels, such as WELDOX 700, NA-XTRA 55, 60, 65 and 70, T1, T1A, T1B, HY80 and HY90. With the correctly selected technological procedure, it may also be suitable for other compatible high-strength structural steels. The specific filler material must always be selected according to the required mechanical properties of the joint and the base material documentation.
Typical application areas include crane booms, hydraulic and construction machinery, earth-moving equipment, lifting devices, heavy steel structures, machine frames and components operating under high loads. The wire is primarily used in mechanical engineering, repair work and the production of special steel structures.
Welding is performed using the MAG (135) process under the protection of a suitable argon and carbon dioxide (Ar/CO2) mixture, typically group M21 according to EN ISO 14175. Direct current with positive polarity of the welding wire DC+ is recommended. When working with high-strength steels, it is important to adhere to the prescribed preheating, interpass temperature and controlled heat input to preserve the mechanical properties of the weld joint and reduce the risk of cracking.
The 1.0 mm diameter wire allows for precise control of the welding process when welding thinner and medium-thickness high-strength steel parts. It is supplied on a D300 spool weighing 16 kg, suitable for professional MIG/MAG welding equipment.
Main advantages:
- Professional low-alloy welding wire ELBOR NiMoCr
- Classification AWS A5.28 ER110S-G
- Designed for MAG welding of high-strength and refined steels
- Alloyed with nickel, molybdenum and chromium
- Suitable for high-strength weld joints
- Good toughness of the weld metal at low temperatures
- Application at temperatures down to approximately -40 °C under approved welding procedure conditions
- Suitable for WELDOX 700 and NA-XTRA steels
- Usable on selected T1, HY80 and HY90 steels
- Designed for the manufacture and repair of crane booms
- Suitable for welding components of construction and earthmoving machinery
- Application in mechanical engineering and the manufacture of high-load steel structures
- Suitable for both manual and mechanised MAG welding
- Welding with Ar/CO2 shielding gas
- Direct current welding DC+
- Diameter 1,0 mm for controlled welding
- Industrial packaging 16 kg on a D300 spool
Classification:
| Standard / Designation | Classification |
|---|---|
| AWS A5.28 | ER110S-G |
| EN ISO 16834-A | The precise classification of ELBOR must be confirmed by the manufacturer's technical data sheet |
| Trade name | ELBOR NiMoCr |
| Filler material type | Low-alloy solid steel welding wire |
| Alloying | Ni-Mo-Cr |
| Welding process | MAG (135) |
| Polarity | DC+ |
Chemical composition:
| Chemical element | Content in ELBOR NiMoCr wire (%) |
|---|---|
| Carbon (C) | Precise value not confirmed |
| Silicon (Si) | Precise value not confirmed |
| Manganese (Mn) | Precise value not confirmed |
| Nickel (Ni) | Alloying element – exact content not confirmed |
| Chromium (Cr) | Alloying element – exact content not confirmed |
| Molybdenum (Mo) | Alloying element – exact content not confirmed |
| Iron (Fe) | Base component |
The numerical values of the chemical composition for the specific ELBOR NiMoCr wire are not sufficiently confirmed in the available documentation. The chemical composition must be supplemented from the manufacturer's technical data sheet or material certificate.
Mechanical properties:
| Mechanical property | Stated value |
|---|---|
| Yield strength Re / Rp0.2 | Min. 690 MPa* |
| Tensile strength Rm | 770–940 MPa* |
| Elongation A5 | Min. 17% |
| Impact energy KV (-40 °C) | Min. 47 J |
| Weld metal condition | As-welded, without additional heat treatment |
*Strength values are provided based on classification-comparable ER110S-G wires and require confirmation by ELBOR documentation. In the current VALTEC description, the yield strength and tensile strength values are likely swapped. The data provided cannot be considered as certified properties of a specific supplied batch.
Do you need advice?
Do you need advice?


Lieskovská cesta 13
962 21 Lieskovec





