


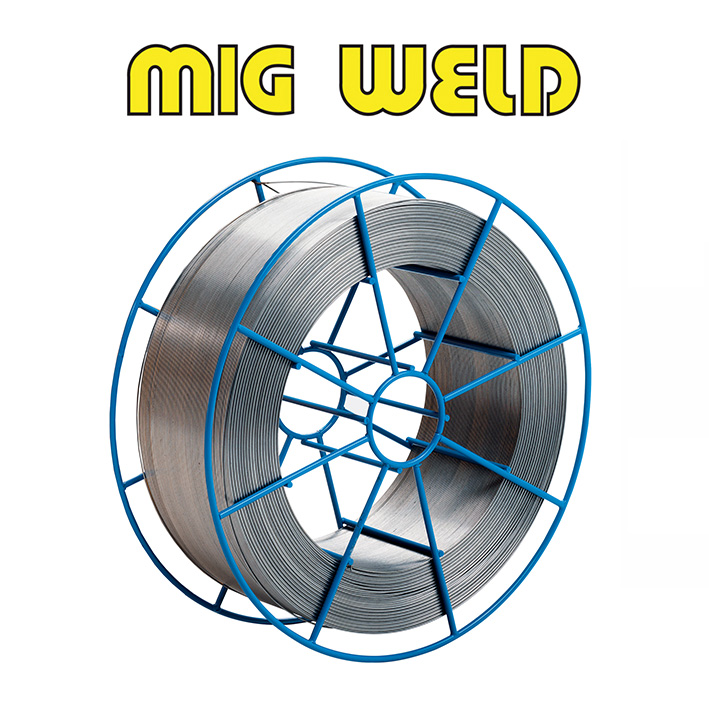
MIG WELD ML5183 (AlMg4,5Mn) Wire 1.0mm/7kg, BS300

Do you need advice?
MIG WELD ML5183 (AlMg4,5Mn) Wire 1.0mm/7kg, BS300
15,56 € incl. tax

MIG WELD ML5183 (AlMg4,5Mn) Wire 1.0 mm / 7 kg / ER5183 / BS300
MIG WELD ML5183 is a solid aluminium welding wire alloyed with magnesium and manganese, designed for MIG welding of aluminium alloys. It complies with EN ISO 18273: S Al 5183 (AlMg4,5Mn0,7) and AWS A5.10: ER5183 classifications, with material number 3.3548. A magnesium content of approximately 4.3–5.2% and manganese of 0.5–1.0% ensures good weld metal strength and high corrosion resistance in marine environments.
The welding wire is intended for joining aluminium alloys that require high strength and resistance to the effects of seawater. It is characterised by good mechanical properties and suitability for welding stressed aluminium structures. It is used with inert shielding gases I1 (argon), I2 (helium) or I3 (argon-helium mixtures) according to EN ISO 14175. Direct current with positive wire polarity (DC+) is used during MIG welding.
MIG WELD ML5183 is used in the manufacture of boats, marine and coastal structures, cryogenic equipment, railway vehicles and automotive components. It is suitable for welding alloys AlMg4,5Mn, AlMg5, AlMg2Mn0,8, AlMgSi0,5, AlMgSi1 and other compatible aluminium materials. A diameter of 1.0 mm allows for precise welding of thin and medium-thickness aluminium parts. The wire is supplied in a 7 kg BS300 spool package, suitable for professional use in metalworking and industrial operations.
Main advantages:
- Aluminium welding wire MIG WELD ML5183
- Classification ER5183 / S Al 5183 / AlMg4,5Mn0,7
- Material number 3.3548
- Magnesium content 4.3–5.2% and manganese 0.5–1.0%
- High weld metal corrosion resistance in seawater
- Good strength and ductility of the weld metal
- Suitable for high-strength stressed aluminium structures
- Designed for MIG welding of aluminium alloys
- Compatible with shielding gases Ar, He and Ar/He
- Suitable for ship structures and marine equipment
- Application in the manufacture of cryogenic equipment and transport technology
- Suitable for welding aluminium alloys of the AlMg series and selected AlMgSi
- Diameter 1.0 mm for controlled welding of aluminium parts
- Professional packaging 7 kg on a BS300 spool
Classification:
| Standard / Designation | Classification |
|---|---|
| EN ISO 18273 | S Al 5183 (AlMg4,5Mn0,7) |
| AWS A5.10 / SFA-5.10 | ER5183 |
| Material number | 3.3548 |
| Trade name | MIG WELD ML5183 |
| Filler material type | Solid aluminium welding wire alloyed with Mg and Mn |
| Welding process | MIG (131) |
Chemical composition:
| Chemical element | Content (%) |
|---|---|
| Magnesium (Mg) | 4.30–5.20 |
| Manganese (Mn) | 0.50–1.00 |
| Chromium (Cr) | 0.05–0.25 |
| Silicon (Si) | Max. 0.40 |
| Iron (Fe) | Max. 0.40 |
| Copper (Cu) | Max. 0.10 |
| Zinc (Zn) | Max. 0.25 |
| Titanium (Ti) | Max. 0.15 |
| Beryllium (Be) | Max. 0.0003 |
| Other elements individually | Max. 0.05 |
| Other elements total | Max. 0.15 |
| Aluminium (Al) | Balance |
Chemical composition according to the MIG WELD ML5183 manufacturer's product documentation. The stated values represent ranges and maximum element contents, not an analysis of a specific production batch.
Mechanical properties:
| Mechanical property | Approximate value |
|---|---|
| Yield strength Rp0.2 | 125 MPa |
| Tensile strength Rm | 275 MPa |
| Elongation A5 | 17 % |
| Mechanical test temperature | +20 °C |
Indicative mechanical properties of the pure weld metal according to MIG WELD ML5183 at a test temperature of +20 °C. Values serve as a technical reference and do not represent guaranteed results for a specific delivered batch.
Do you need advice?
Alternative goods
 Drôt MIG ALUNOX AlMg4,5Mn 1,2mm/7kg (1.5183)
15,99 € incl. tax
MIG wire ALUNOX AlMg4,5Mn 1,0mm/7kg (1.5183)
16,73 € incl. tax
 Drôt MIG ELBOR AlMg4,5Mn 1,2mm /7kg (1.5183) D-300
14,37 € incl. tax
MIG wire ELBOR AlMg4,5Mn 1,0/7kg (1.5183) D-300
14,33 € incl. tax
Do you need advice?


Lieskovská cesta 13
962 21 Lieskovec





