


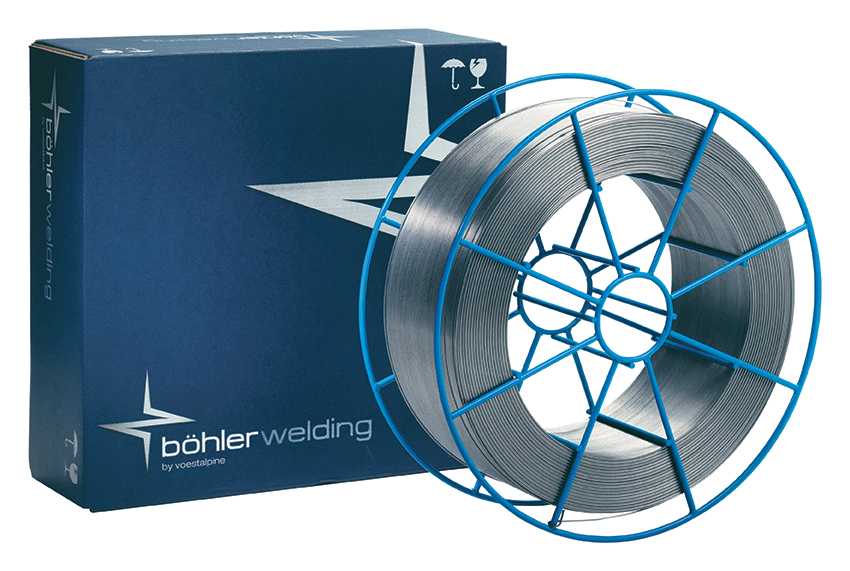
MIG wire BOHLER AWS ER316LSi 1.2mm/15kg (86259)

Do you need advice?
MIG wire BOHLER AWS ER316LSi 1.2mm/15kg (86259)
 Drôt MIG BOHLER AWS ER316LSi 0,8mm/15kg (85518)
25,14 € incl. tax
 Drôt MIG BOHLER AWS ER316LSi 1,0mm/15kg (86258)
15,58 € incl. tax
 Drôt MIG BOHLER AWS ER316LSi 1,2mm/15kg (86259)
15,10 € incl. tax
15,10 € incl. tax

BÖHLER AWS ER316LSi MIG wire 1.2 mm / 15 kg (86259)
BÖHLER AWS ER316LSi MIG wire is a high-alloy solid stainless steel welding wire intended for MAG welding of austenitic stainless steels of types 316, 316L and 316Ti. It corresponds to the AWS A5.9: ER316LSi and EN ISO 14343-A: G 19 12 3 L Si classifications. The material designation of the filler material is 1.4430.
The wire is alloyed with chromium, nickel and molybdenum (Cr-Ni-Mo), which ensure good corrosion resistance of the weld metal. Molybdenum increases resistance to local and pitting corrosion compared to ER308LSi wires. Low carbon content reduces the risk of intercrystalline corrosion, and increased silicon content improves weld metal fluidity, wetting of the weld edges and the uniformity of the weld bead.
BÖHLER ER316LSi provides good feeding properties, stable welding and a high-quality weld appearance. The manufacturer states corrosion resistance of the weld metal at operating temperatures up to +400 °C and the possibility of use at low temperatures down to -196 °C. Such applications must comply with the requirements for the base material, mechanical properties and a qualified welding procedure.
The welding wire is suitable for steels 1.4401 (AISI 316), 1.4404 (AISI 316L), 1.4435, 1.4436, 1.4571 (AISI 316Ti), 1.4580 and 1.4583, as well as selected corrosion-resistant steel castings. It is used in the production of stainless steel pipes, pressure vessels, tanks, technological piping, heat exchangers, machine parts and industrial structures.
It finds application primarily in the chemical, food, pharmaceutical, energy and engineering industries, where a high-quality welded joint with good corrosion resistance is required. Suitability for specific aggressive environments or contact with chlorides must be assessed according to the operating conditions.
Welding is carried out using the MAG (135) process with an argon-based shielding gas with a maximum of 2.5% CO2, according to the manufacturer's technical data sheet. Direct current with positive wire polarity DC+ is used. When welding stainless steels, it is necessary to ensure material purity, limit excessive heat input and use root protection of the weld depending on the type of joint.
The diameter of 1.2 mm provides good deposition rates and is suitable for productive welding of medium and thick stainless steel parts. The wire is supplied in 15 kg spool packaging, suitable for professional and industrial MIG/MAG welding equipment.
Main advantages:
- Professional stainless steel welding wire BÖHLER AWS ER316LSi
- Classification AWS A5.9 ER316LSi
- Classification EN ISO 14343-A G 19 12 3 L Si
- Material designation 1.4430
- Designed for MAG welding of austenitic stainless steels
- Suitable for steels 316, 316L and 316Ti
- Alloyed with chromium, nickel and molybdenum
- Low carbon content reducing the risk of intercrystalline corrosion
- Molybdenum improving resistance to pitting corrosion
- Increased silicon content improving the flowability of the weld metal
- Good wetting of the weld edges and a uniform weld appearance
- Very good feeding properties
- Corrosion resistance of the weld metal at operating temperatures up to +400 °C
- Possibility of use at low temperatures down to -196 °C
- Suitable for stainless steel pipes, tanks and pressure equipment
- Application in the chemical, food and pharmaceutical industries
- Welding with shielding gas Ar + max. 2.5% CO2
- Direct current welding DC+
- Diameter 1.2 mm for productive MAG welding
- Industrial packaging 15 kg on a spool
Classification:
| Standard / Designation | Classification |
|---|---|
| AWS A5.9 / SFA-5.9 | ER316LSi |
| EN ISO 14343-A | G 19 12 3 L Si |
| EN ISO 14343-B | SS316LSi |
| Material number | 1.4430 |
| Trade name | BÖHLER AWS ER316LSi |
| Weld metal type | Austenitic Cr-Ni-Mo, low carbon |
| Welding process | MAG (135) |
| Polarity | DC+ |
Chemical composition:
| Chemical element | Typical content (%) |
|---|---|
| Carbon (C) | 0,02 |
| Silicon (Si) | 0,80 |
| Manganese (Mn) | 1,70 |
| Chromium (Cr) | 18,40 |
| Nickel (Ni) | 12,40 |
| Molybdenum (Mo) | 2,80 |
| Iron (Fe) | Balance |
Typical chemical composition of the solid wire according to the BÖHLER AWS ER316LSi (02/2016) technical data sheet. Values do not represent a chemical analysis of a specific production batch.
Mechanical properties:
| Mechanical property | Typical value | Minimum value |
|---|---|---|
| Yield strength Rp0.2 | 420 MPa | 320 MPa |
| Tensile strength Rm | 560 MPa | 510 MPa |
| Elongation A5 | 35 % | 25 % |
| Impact energy KV (+20 °C) | 70 J | Not specified |
| Impact energy KV (-196 °C) | Min. 32 J | |
| Weld metal condition | As-welded, without additional heat treatment | |
| Shielding gas during test | Ar + 2.5 % CO2 | |
Mechanical properties of the pure weld metal according to the BÖHLER AWS ER316LSi (02/2016) technical data sheet, tested with Ar + 2.5% CO2 shielding gas. These are typical and declared minimum values according to the documentation, not the test results of a specific delivered batch.
Do you need advice?
Alternative goods
 Drôt MIG BOHLER Q G 316LSi 0,8mm /15kg (72116)
27,23 € incl. tax
 Drôt MIG BOHLER Q G 316LSi 1,0mm/15kg (72117)
23,54 € incl. tax
MIG wire BOHLER QG 316LSi 1.2mm/15kg (72118)
23,12 € incl. tax
MIG wire BOHLER Thermanit GE-316LSi 1.2mm/15kg (1.4430) (45569)
20,66 € incl. tax
13,16 € incl. tax
Wire MIG STAVINOX ER 316LSi 1.2mm/15kg (1.4430) BS300
13,04 € incl. tax
Do you need advice?


Lieskovská cesta 13
962 21 Lieskovec





