


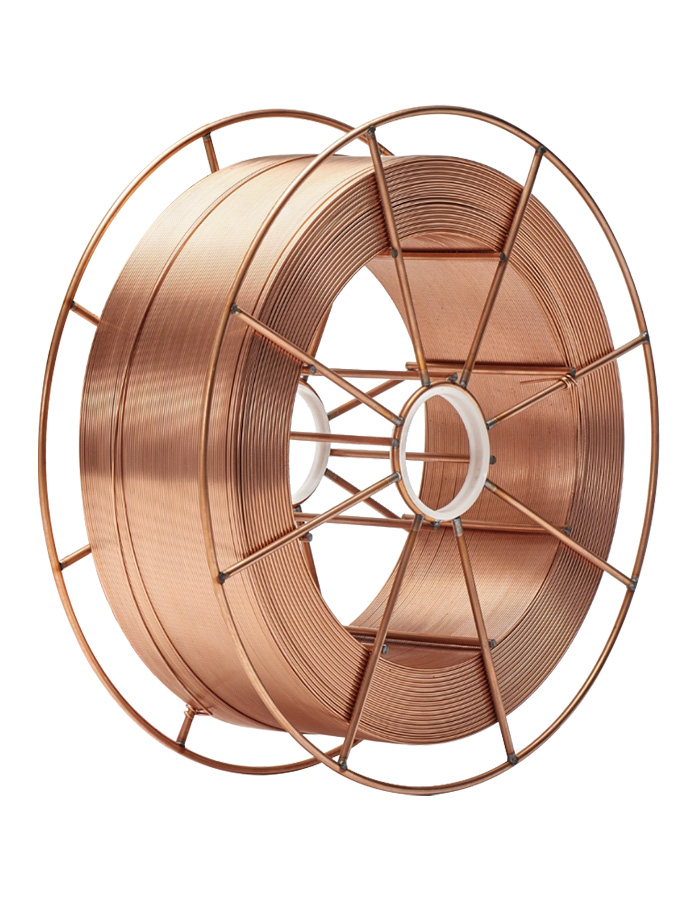
MIG WELD SG3 ECO Wire 1.0mm /15kg JQ MG50-6AN GOLDEN BRIDGE (G4Si1) BS300, Uncoated

Do you need advice?
MIG WELD SG3 ECO Wire 1.0mm /15kg JQ MG50-6AN GOLDEN BRIDGE (G4Si1) BS300, Uncoated
2,92 € incl. tax

MIG WELD SG3 ECO Wire 1.0 mm / 15 kg JQ MG50-6AN GOLDEN BRIDGE (G4Si1) BS300 – uncoppered
The MIG WELD SG3 ECO JQ MG50-6AN wire from GOLDEN BRIDGE is an uncoppered solid welding wire designed for MAG welding of non-alloy and low-alloy structural steels. It corresponds to classification SG3 / G4Si1 / ER70S-6. Thanks to its higher manganese and silicon content, it provides excellent deoxidation properties, a stable welding arc, and high-quality weld metal with good strength and toughness.
The characteristic feature of the JQ MG50-6AN version is a surface without an additional copper layer. The wire is characterised by smooth feeding, low spatter formation, and a uniform appearance of the weld bead. According to the manufacturer, it exhibits good tolerance to mill scale and slight surface contamination of the base material, as well as low sensitivity to porosity. It is suitable for welding in all common welding positions using CO2 (C1) shielding gas or an Ar/CO2 mixture (M21).
The wire is suitable for welding structural, fine-grained and selected low-alloy steels with a strength class of approximately 500 MPa. It is used in the production of steel structures, bridges, frames, machine components, transport equipment, trailers, tanks and industrial equipment. The 1.0 mm diameter provides a good compromise between deposition rate and weld pool control. The 15 kg BS300 spool is designed for regular use in metal fabrication, locksmith workshops, and industrial operations.
Main advantages:
- Solid uncoppered welding wire GOLDEN BRIDGE JQ MG50-6AN
- Classification SG3 / G4Si1 / ER70S-6
- Designed for MAG welding of non-alloy and low-alloy steels
- Surface without an additional copper layer
- Higher manganese and silicon content for good deoxidation properties
- Stable welding arc and low spatter formation
- Good feeding characteristics and a uniform weld appearance
- Low sensitivity to porosity under correct welding conditions
- Good strength and toughness of the weld metal
- Suitable for welding in all common welding positions
- Option to use shielding gases C1 (CO2) and M21 (Ar/CO2)
- Suitable for steel structures, frames, and mechanical engineering
- Diameter 1.0 mm for universal welding of steel parts
- Industrial packaging 15 kg on a BS300 spool
Classification:
| Standard / Designation | Classification |
|---|---|
| EN ISO 14341-A (C1) | G 42 4 C1 4Si1 |
| EN ISO 14341-A (M21) | G 46 5 M21 4Si1 |
| AWS A5.18 | ER70S-6 |
| JIS | YGW12 |
| Trade name | SG3 ECO / G4Si1 / JQ MG50-6AN |
| Surface Treatment | Non-coppered |
| Filler material type | Solid steel welding wire without a copper surface layer |
| Welding process | MAG (135) |
Chemical composition:
| Chemical element | Content (%) |
|---|---|
| Carbon (C) | 0,075 |
| Silicon (Si) | 0,94 |
| Manganese (Mn) | 1,76 |
| Phosphorus (P) | 0,014 |
| Sulphur (S) | 0,012 |
| Nickel (Ni) | 0,013 |
| Chromium (Cr) | 0,010 |
| Molybdenum (Mo) | 0,004 |
| Vanadium (V) | 0,001 |
| Copper (Cu) | 0,015 |
| Iron (Fe) | Balance |
Example chemical composition of the JQ MG50-6AN welding wire according to the manufacturer GOLDEN BRIDGE. Values do not represent an analysis of a specific production batch.
Mechanical properties:
| Mechanical property | C1 (CO2) | M21 (Ar/CO2) |
|---|---|---|
| Yield strength Re / Rp0.2 | 460 MPa | 495 MPa |
| Tensile strength Rm | 562 MPa | 587 MPa |
| Elongation A | 28 % | 28,5 % |
| KV2 test temperature | -40 °C | -50 °C |
| Impact energy KV2 | 78 / 79 / 89 J | 82 / 85 / 71 J |
Example test results of all-weld metal according to GOLDEN BRIDGE for shielding gases C1 and M21. Testing temperatures are -40 °C for C1 and -50 °C for M21. The values stated are not the results of a test from a specific delivered batch.
Do you need advice?
Alternative goods
MIG wire ELBOR SG3 SOLUTION 3 1.0mm /16kg G4Si1 uncoppered
3,19 € incl. tax
MIG wire BOHLER ECOspark 460 1.0mm /18kg (SG3/G4Si1) 63318 uncoppered
2,82 € incl. tax
MIG wire BOHLER ECOspark 460 1.0mm /250kg (SG3/G4Si1) (63400) copper-free
2,92 € incl. tax
4,03 € incl. tax
MIG wire BOHLER EMK 8 NC 1.0mm /18kg (G4Si1) (27460) uncoppered
3,96 € incl. tax
Do you need advice?


Lieskovská cesta 13
962 21 Lieskovec





