


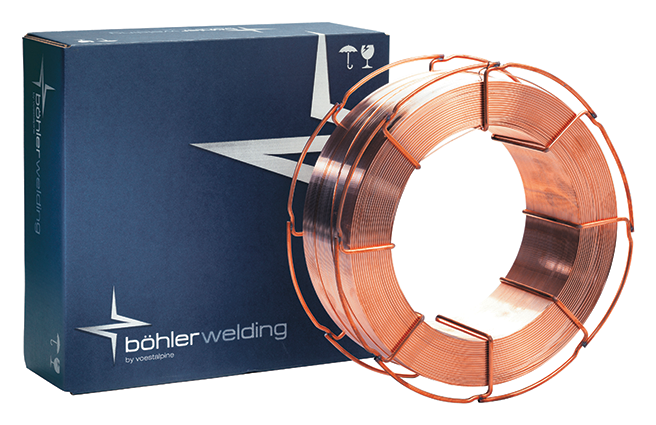
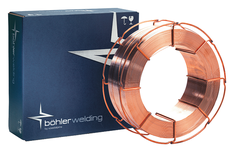
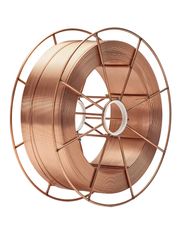
MIG wire BOHLER EMK 8 NC 1.2mm /18kg (G4Si1) (27463) uncoppered

Do you need advice?
MIG wire BOHLER EMK 8 NC 1.2mm /18kg (G4Si1) (27463) uncoppered
4,03 € incl. tax
3,96 € incl. tax
3,92 € incl. tax

BÖHLER EMK 8 NC MIG Wire 1.2 mm / 18 kg (SG3/G4Si1) – non-copper coated (27463)
BÖHLER EMK 8 NC MIG wire is a professional non-copper coated solid welding wire designed for MAG welding of unalloyed and fine-grain structural steels. It corresponds to classification EN ISO 14341-A: G 46 4 M21 4Si1 / G 46 4 C1 4Si1 and AWS A5.18: ER70S-6. It belongs to the SG3/G4Si1 group and, thanks to its increased manganese and silicon content, provides good deoxidising properties, strength, and toughness of the weld metal.
The main advantage of the BÖHLER EMK 8 NC wire is its specially treated non-copper coated surface, which ensures excellent feeding properties even at high feed speeds. The wire creates a very stable welding arc with extremely low spatter formation and limited formation of oxides and silicate deposits on the weld bead surface. These properties contribute to a reduced need for subsequent cleaning of weld joints and higher welding productivity.
The wire is suitable for manual, mechanised, and robotic welding using shielding gases of classes C1, M2, and M3 according to EN ISO 14175. Pure carbon dioxide CO2 or suitable argon-based mixed shielding gases can be used. Welding is carried out with direct current and positive polarity of the welding wire DC+.
BÖHLER EMK 8 NC is intended for welding steels with a yield strength of up to approximately 460 MPa. It is suitable for structural steels S235JR, S275JR, S355JR, S355J2, S460N, and S460M, pressure steels P235GH to P355GH, selected pipe steels, and other compatible unalloyed and fine-grain steels. It is used in the production of steel structures, frames, beams, pressure vessels, boilers, machine parts, transport equipment and industrial welded assemblies.
The diameter of 1.2 mm enables productive welding of medium-thick and thicker steel parts. The wire is supplied in 18 kg spools, designed for professional and industrial welding equipment. Thanks to stable feeding and low spatter formation, it is also suitable for automated and robotic workstations.
Main advantages:
- Professional welding wire BÖHLER EMK 8 NC
- Non-copper coated surface without an additional copper layer
- Classification SG3 / G4Si1 / ER70S-6
- Designed for MAG welding of non-alloy and fine-grained steels
- Excellent feeding properties even at high feed speeds
- Very stable welding arc
- Extremely low spatter formation during welding
- Limited formation of oxides and silicate deposits on the weld surface
- Reduced need for subsequent cleaning of welded joints
- Good deoxidising properties thanks to manganese and silicon
- High strength and toughness of the weld metal
- Typical tensile strength 620 MPa
- Typical impact energy 80 J at -40 °C
- Option to use shielding gases C1, M2 and M3
- Suitable for manual, mechanised and robotic welding
- Use for steel structures, pressure vessels and machine parts
- Diameter 1.2 mm for productive MAG welding
- Industrial packaging 18 kg on spool
Classification:
| Standard / Designation | Classification |
|---|---|
| EN ISO 14341-A (M21) | G 46 4 M21 4Si1 |
| EN ISO 14341-A (C1) | G 46 4 C1 4Si1 |
| AWS A5.18 / SFA-5.18 | ER70S-6 |
| Trade name | BÖHLER EMK 8 NC |
| Material group | SG3 / G4Si1 |
| Surface Treatment | Non-coppered |
| Filler material type | Solid steel welding wire |
| Welding process | MAG (135) |
Chemical composition:
| Chemical element | Typical content (%) |
|---|---|
| Carbon (C) | 0,10 |
| Silicon (Si) | 1,00 |
| Manganese (Mn) | 1,70 |
| Iron (Fe) | Balance |
Typical chemical composition of the solid wire according to the BÖHLER EMK 8 NC (03/2017) technical data sheet. This is not a chemical analysis of a specific production batch.
Mechanical properties:
| Mechanical property | Typical value | Minimum value / range |
|---|---|---|
| Yield Strength Re | 480 MPa | Min. 460 MPa |
| Tensile strength Rm | 620 MPa | 530–680 MPa |
| Elongation A5 | 26 % | Not specified separately |
| Impact energy KV (+20 °C) | 150 J | Not specified separately |
| Impact energy KV (-40 °C) | 80 J | Min. 47 J |
| Weld metal condition | As-welded, without additional heat treatment | |
Reference mechanical properties of the pure weld metal according to the BÖHLER EMK 8 NC (03/2017) technical data sheet, using shielding gas M21 or CO2. Actual results depend on the welding conditions and the specific batch.
Do you need advice?
Alternative goods
3,96 € incl. tax
MIG wire BOHLER EMK 8 NC SG3 1.0mm/250kg (G4Si1) (27467) copper-free
4,03 € incl. tax
4,03 € incl. tax
MIG wire BOHLER EMK 8 NC SG3 1.2mm /250kg (G4Si1) (27469) uncoppered
4,00 € incl. tax
4,03 € incl. tax
MIG wire BOHLER EMK 8 NC 1.2mm /18kg (G4Si1) (27463) uncoppered
3,92 € incl. tax
4,03 € incl. tax
MIG wire BOHLER EMK 8 NC 1.0mm /18kg (G4Si1) (27460) uncoppered
3,96 € incl. tax
MIG wire BOHLER ECOspark 460 1.2mm /18kg (SG3/G4Si1) (63351) copper-free
2,78 € incl. tax
MIG Wire BOHLER ECOspark 8-NC SG3 1.2mm /250kg (G4Si1) (85978) Uncoated
3,20 € incl. tax
MIG wire BOHLER EMK 8 SG3 1.2/18kg (G4Si1) 71296
3,44 € incl. tax
MIG wire BOHLER EMK 8 SG3 1.2mm /250kg (G4Si1) (56558)
3,91 € incl. tax
MIG wire ELBOR SG3 1.2/250kg G4Si1 (3FUS12KG250)
2,77 € incl. tax
MIG wire ELBOR SG3 1.2/16kg G4Si1 (3SPF12KG16)
2,74 € incl. tax
MIG wire ELBOR SG3 SOLUTION 3 1.2mm /16kg G4Si1 uncoppered
3,36 € incl. tax
MIG Wire ELBOR SG3 SOLUTION 3 1.2mm /250kg G4Si1 Uncoated
2,80 € incl. tax
MIG WELD SG3 Wire 1.2mm /15kg JQ MG50-6A GOLDEN BRIDGE (G4Si1) BS300
2,77 € incl. tax
MIG WELD SG3 ECO Wire 1.2mm /15kg JQ MG50-6AN GOLDEN BRIDGE(G4Si1) BS300, uncoppered
2,89 € incl. tax
Do you need advice?


Lieskovská cesta 13
962 21 Lieskovec





