


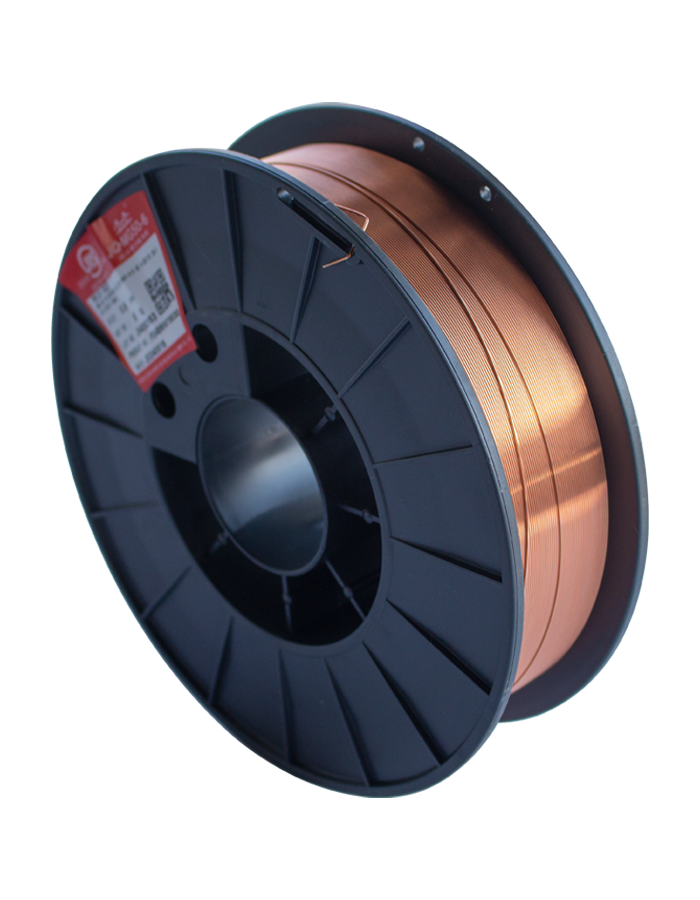
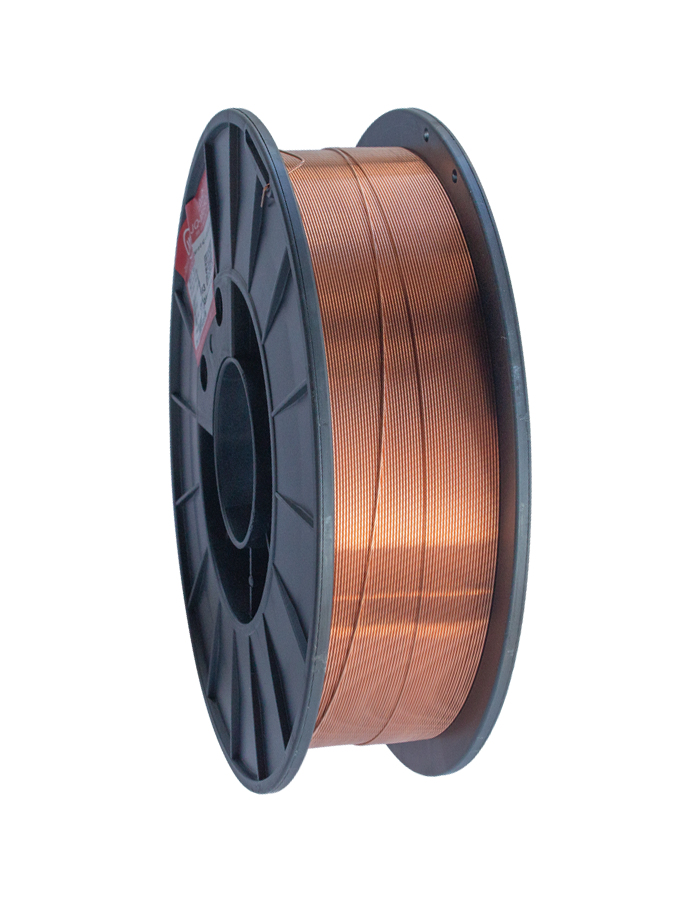
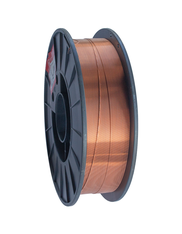
MIG Wire WELD SG2 1.0 mm/5 kg JQ MG50-6 GOLDEN BRIDGE (G3Si1) D200

Do you need advice?
MIG Wire WELD SG2 1.0 mm/5 kg JQ MG50-6 GOLDEN BRIDGE (G3Si1) D200
 0.8 mm
4,80 € incl. tax
 1.0 mm
4,55 € incl. tax
 0.6 mm
6,15 € incl. tax
4,55 € incl. tax

MIG WELD SG2 Wire 1.0 mm / 5 kg JQ MG50-6 GOLDEN BRIDGE (G3Si1) D200
MIG WELD SG2 JQ MG50-6 GOLDEN BRIDGE is a professional copper-coated solid steel welding wire intended for MAG welding of non-alloy and low-alloy structural steels. It complies with classification EN ISO 14341-A: G 42 4 C1/M21 3Si1 and AWS A5.18: ER70S-6. It belongs to the SG2 / G3Si1 material group and is suitable for both general and professional welding applications.
The wire is alloyed with manganese and silicon, which ensure good deoxidation properties and contribute to achieving high-quality welded joints. Copper surface layer helps protect the wire from surface oxidation and supports reliable welding current transfer through the contact tip.
The manufacturer GOLDEN BRIDGE states very good welding properties: a stable electric arc, low spatter formation, smooth feeding, and a uniform appearance of the weld bead. The wire can be used for welding in all common welding positions. It also features low sensitivity to pore formation and good tolerance to mill scale residues and oil contaminants on the surface of the base material. However, it is recommended to thoroughly clean the welding surfaces before welding.
JQ MG50-6 wire is intended for welding carbon and low-alloy steels with a tensile strength of approximately 500 MPa. It is particularly suitable for structural steels S235, S275 and S355 and other compatible materials according to the required mechanical properties of the welded joint.
It is used in the production of steel structures, bridge elements, beams, frames, automotive parts, machine components, metal assemblies and for general locksmith work. It is suitable for welding butt and fillet joints, manual and mechanised welding, and multi-pass welded joints according to the technological procedure.
Welding is performed using the MAG (135) process with a shielding gas of 100% CO2 (C1) or a mixture of argon and carbon dioxide (M21) according to EN ISO 14175. Direct current with positive wire polarity DC+ is used.
The 1.0 mm diameter provides a good compromise between weld pool control and deposition rate. The manufacturer recommends a welding current of 50–220 A and, when welding with CO2, a shielding gas flow rate of approximately 15–20 l/min. The precise setting of the welding voltage depends on the material thickness, welding position, and the equipment used.
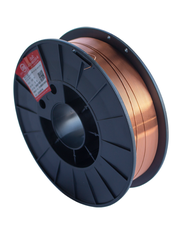
The wire is supplied in a 5 kg pack on a D200 spool, which is suitable for many compact and professional MIG/MAG welding machines that support this spool size. The packaging is practical for workshops, assembly, service work, and smaller production facilities.
Main advantages:
- Professional welding wire GOLDEN BRIDGE JQ MG50-6
- Classification SG2 / G3Si1 / AWS ER70S-6
- Copper-coated surface for reliable current transfer
- Designed for MAG welding of non-alloy and low-alloy steels
- Stable electric arc
- Low spatter formation
- Smooth and reliable wire feeding
- Uniform and aesthetic appearance of the weld bead
- Good deoxidising properties thanks to manganese and silicon
- Good tolerance to mill scale residues on the steel surface
- Low sensitivity to pore formation under correct welding conditions
- Capable of welding in all common positions
- Suitable for S235, S275 and S355 steels
- Applied in the production of bridges, frames and steel structures
- Suitable for bodywork and engineering works
- Usable for manual and mechanised welding
- Shielding gas CO2 or Ar/CO2
- Direct current welding DC+
- Recommended welding current 50–220 A
- Diameter 1.0 mm for universal MAG welding
- Practical packaging: 5 kg on a D200 spool
Classification:
| Standard / Designation | Classification |
|---|---|
| EN ISO 14341-A | G 42 4 C1 3Si1 / G 42 4 M21 3Si1 |
| AWS A5.18 | ER70S-6 |
| JIS | YGW12 |
| Material group | SG2 / G3Si1 |
| Trade name | JQ MG50-6 |
| Filler material type | Copper-coated solid steel welding wire |
| Welding process | MAG (135) |
| Shielding gas | C1 / M21 |
| Polarity | DC+ |
Chemical composition:
| Chemical element | Typical content (%) |
|---|---|
| Carbon (C) | 0,077 |
| Manganese (Mn) | 1,54 |
| Silicon (Si) | 0,88 |
| Sulphur (S) | 0,011 |
| Phosphorus (P) | 0,012 |
| Nickel (Ni) | 0,011 |
| Chromium (Cr) | 0,020 |
| Molybdenum (Mo) | 0,008 |
| Vanadium (V) | 0,001 |
| Copper (Cu) | 0,14 |
| Iron (Fe) | Balance |
Example of the chemical composition of JQ MG50-6 welding wire according to the manufacturer TIANJIN GOLDEN BRIDGE. Values represent a reference analysis, not the chemical composition of a specific delivered batch.
Mechanical properties:
| Mechanical property | Guaranteed value | Example of measured value |
|---|---|---|
| Yield strength Re / Rp0.2 | ≥ 420 MPa | 450 MPa |
| Tensile strength Rm | 520–640 MPa | 555 MPa |
| Elongation A | ≥ 22% | 29 % |
| Impact energy KV (-40 °C) | ≥ 47 J | 77 / 95 / 83 J |
| Weld metal condition | As-welded, without subsequent heat treatment | |
Mechanical properties of the pure weld metal according to the manufacturer GOLDEN BRIDGE for JQ MG50-6. The stated reference results may vary depending on the shielding gas and welding conditions.
Do you need advice?
Alternative goods
MIG wire BOHLER ECOspark 420 1.0mm /18kg (SG2/G3Si1) 62154 copper-free
2,76 € incl. tax
MIG wire BOHLER EMK 6 SG2 1.0mm /18kg (G3Si1) 71290
3,76 € incl. tax
MIG wire BOHLER EMK 6 SG2 1.0mm /250kg (G3Si1) (56545)
2,80 € incl. tax
MIG wire BOHLER EMK 6-D SG2 1.0mm/15kg (G3Si1) (71363)
3,76 € incl. tax
MIG wire BOHLER EMK 6-D SG2 1.0mm/18kg (G3Si1) (71502)
3,76 € incl. tax
MIG Wire BOHLER EMK 6-Ultra 1,0mm /18kg (SG2/G3Si1) 89151
2,83 € incl. tax
MIG Wire ELBOR BRONZATO SG2 1.0 /250kg G3Si1 (2FUS10KG250BR)
2,68 € incl. tax
 Drôt MIG ELBOR BRONZATO SG2 1,2/16kg
2,61 € incl. tax
MIG wire ELBOR BRONZATO SG2 1.0/16kg G3Si1 (2SPF10KG16BR)
2,66 € incl. tax
2,95 € incl. tax
MIG wire ELBOR SG2 1.0/16kg G3Si1 (2SPF10KG16)
2,71 € incl. tax
MIG wire ELBOR SG2 1.0/250kg G3Si1 (2FUS10KG250)
2,73 € incl. tax
Do you need advice?


Lieskovská cesta 13
962 21 Lieskovec





