


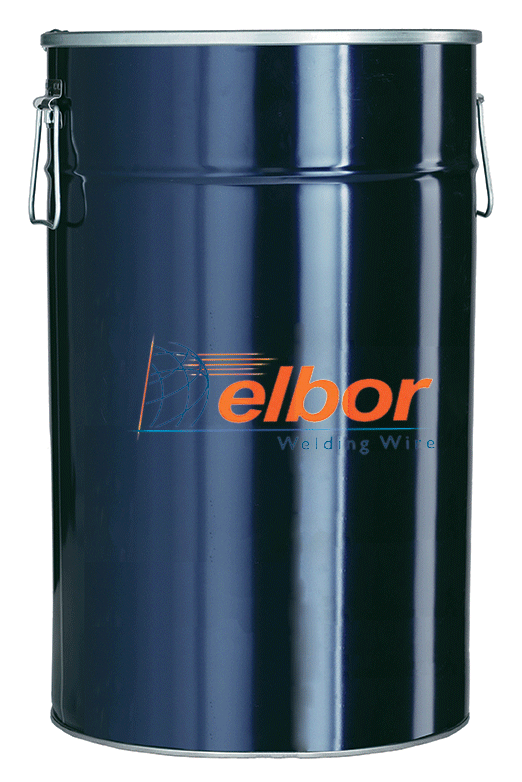
MIG wire ELBOR SG2 1.0/250kg G3Si1 (2FUS10KG250)

Do you need advice?
MIG wire ELBOR SG2 1.0/250kg G3Si1 (2FUS10KG250)
| Quantity | PriceUnit price | Discount % |
|---|---|---|
| 250500kg | 648,38 €2,59 € | 5% |
2,73 € incl. tax

MIG wire ELBOR SG2 1.0 mm / 250 kg G3Si1 – DRUM (2FUS10KG250)
ELBOR SG2 wire is a copper-coated solid welding wire intended for MAG welding of unalloyed and low-alloy structural steels. It corresponds to the classification EN ISO 14341-A: G 42 4 M21 3Si1 / G 38 2 C1 3Si1 and AWS A5.18: ER70S-6. The manganese and silicon content ensures good deoxidation properties, welding arc stability and the required mechanical properties of the weld metal.
The wire is characterised by a stable welding arc, low spatter formation and a uniform weld bead appearance. The copper-coated surface ensures reliable electrical contact with the welding tip and smooth wire feeding through the welding torch. Protective gas C1 (100% CO2) or M21 (Ar/CO2 mixture) is used for welding. The wire is suitable for manual, mechanised and automated MAG welding with direct current and positive wire polarity (DC+).
ELBOR SG2 is suitable for welding structural steels S235, S275 and S355 and other compatible unalloyed carbon steels including ASTM A516 Grade 60. It is used in the manufacture of steel structures, frames, beams, pipes, tanks, automotive components and machine parts. The 1.0 mm diameter provides good weld pool control and universal application when welding thinner and medium-thick steel parts.
The wire is supplied in a large-capacity DRUM packaging weighing 250 kg, which is intended primarily for industrial, automated and robotic welding workstations. The large pack allows for longer continuous operation without frequent wire changes, reducing downtime in series production and increasing welding efficiency. A compatible wire feeding and guiding system is required for the use of drum packaging.
Main advantages:
- Copper-coated solid welding wire ELBOR SG2
- Classification SG2 / G3Si1 / ER70S-6
- Designed for MAG welding of non-alloy and low-alloy steels
- Stable welding arc and low spatter formation
- Uniform weld bead appearance
- Copper-coated surface supporting electrical contact and smooth feeding
- Good deoxidation properties thanks to the manganese and silicon content
- Good strength and toughness of the weld metal
- Compatible with protective gases M21 (Ar/CO2) and C1 (CO2)
- Suitable for welding in all common welding positions
- Suitable for structural steels S235, S275 and S355
- Application in the manufacture of steel structures, frames and tanks
- Diameter 1.0 mm for universal MAG welding
- Welding current range 80–250 A according to the manufacturer
- High-capacity packaging DRUM 250 kg
- Suitable for automated and robotic welding
- Less frequent wire changes and shorter downtime during mass production
Classification:
| Standard / Designation | Classification |
|---|---|
| EN ISO 14341-A (M21) | G 42 4 M21 3Si1 |
| EN ISO 14341-A (C1) | G 38 2 C1 3Si1 |
| AWS A5.18 / SFA-5.18 | ER70S-6 |
| Trade name | ELBOR SG2 / ELB-SG2 |
| Material group | SG2 / G3Si1 |
| Surface Treatment | Copper-plated |
| Filler material type | Solid steel welding wire |
| Welding process | MAG (135) |
Chemical composition:
| Chemical element | Typical content (%) |
|---|---|
| Carbon (C) | 0,09 |
| Silicon (Si) | 0,85 |
| Manganese (Mn) | 1,60 |
| Iron (Fe) | Balance |
Typical chemical composition of the weld metal according to the ELBOR SG2 technical data sheet. Values do not represent an analysis of a specific production batch.
Mechanical properties:
| Mechanical property | M21 (Ar/CO2) | C1 (CO2) |
|---|---|---|
| Yield strength Rs | ≥ 420 MPa | ≥ 400 MPa |
| Tensile strength Rm | 500–640 MPa | 480–600 MPa |
| Elongation A5 | ≥ 22% | ≥ 22% |
| Impact energy KV | ≥ 47 J at -40 °C | ≥ 47 J at -20 °C |
Reference mechanical properties of the pure weld metal according to the ELBOR SG2 technical data sheet, distinguished by the protective gas. The values do not constitute a certificate for a specific delivered batch.
Do you need advice?
Alternative goods
MIG wire BOHLER EMK 6 SG2 1.0mm /18kg (G3Si1) 71290
3,76 € incl. tax
MIG wire BOHLER EMK 6 SG2 1.0mm /250kg (G3Si1) (56545)
2,80 € incl. tax
MIG wire BOHLER EMK 6-D SG2 1.0mm/15kg (G3Si1) (71363)
3,76 € incl. tax
MIG wire BOHLER EMK 6-D SG2 1.0mm/18kg (G3Si1) (71502)
3,76 € incl. tax
MIG Wire ELBOR BRONZATO SG2 1.0 /250kg G3Si1 (2FUS10KG250BR)
2,68 € incl. tax
 Drôt MIG ELBOR BRONZATO SG2 1,2/16kg
2,61 € incl. tax
MIG wire ELBOR BRONZATO SG2 1.0/16kg G3Si1 (2SPF10KG16BR)
2,66 € incl. tax
2,95 € incl. tax
MIG wire ELBOR SG2 1.0/16kg G3Si1 (2SPF10KG16)
2,71 € incl. tax
 0.8 mm
2,89 € incl. tax
 1.2 mm
2,71 € incl. tax
Wire MIG WELD SG2 1.0 mm /15 kg JQ MG50-6 GOLDEN BRIDGE (G3Si1) BS300
2,76 € incl. tax
 1,2/250 kg
2,73 € incl. tax
Wire MIG WELD SG2 1.0mm /250kg JQ MG50-6 GOLDEN BRIDGE (G3Si1) barrel
2,78 € incl. tax
 0.8 mm
4,80 € incl. tax
 0.6 mm
6,15 € incl. tax
MIG Wire WELD SG2 1.0 mm/5 kg JQ MG50-6 GOLDEN BRIDGE (G3Si1) D200
4,55 € incl. tax
Do you need advice?


Lieskovská cesta 13
962 21 Lieskovec





